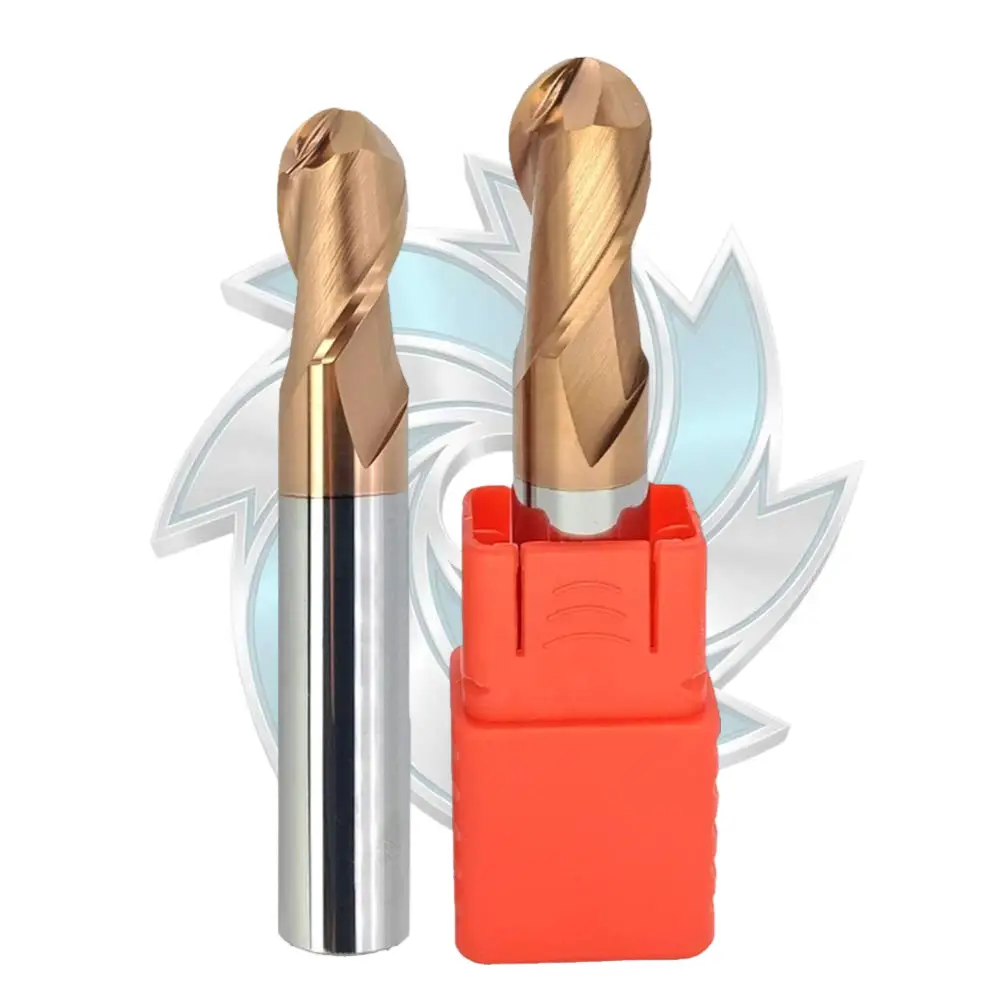
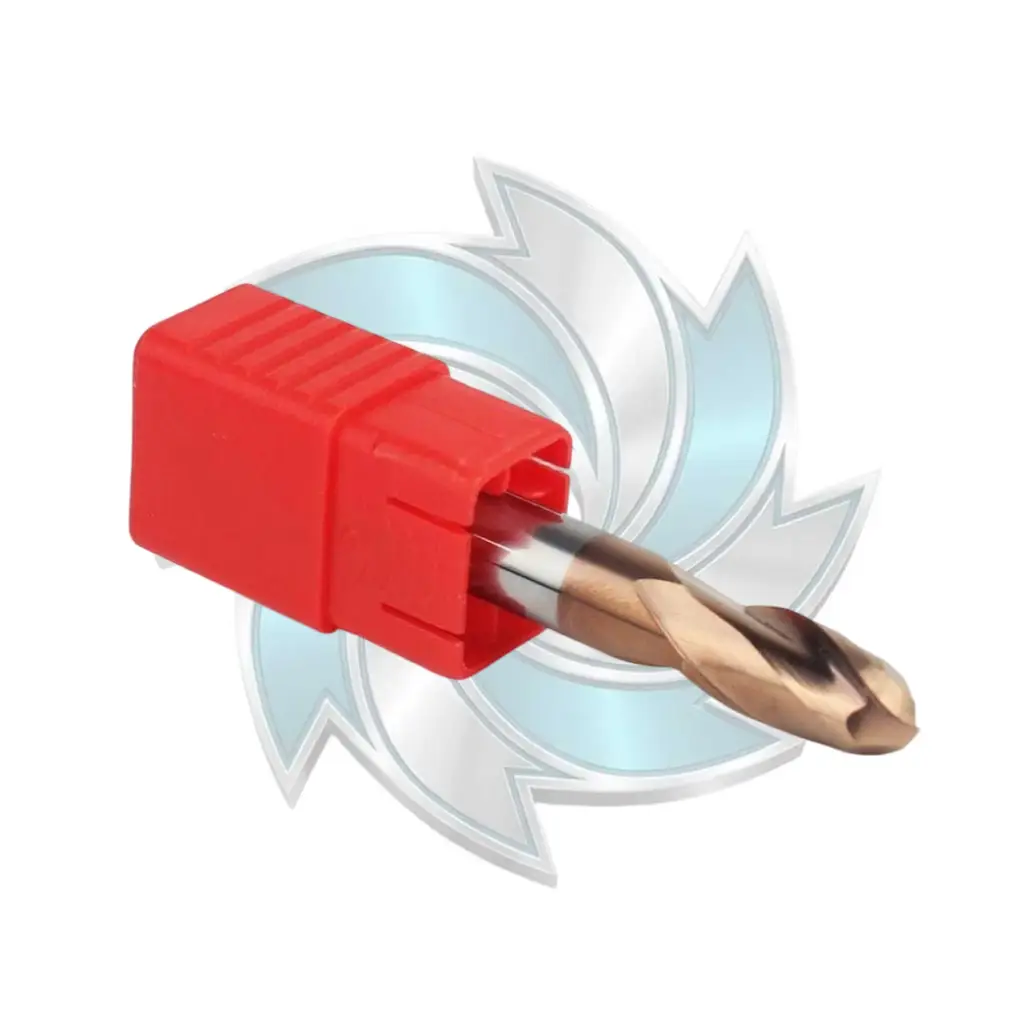
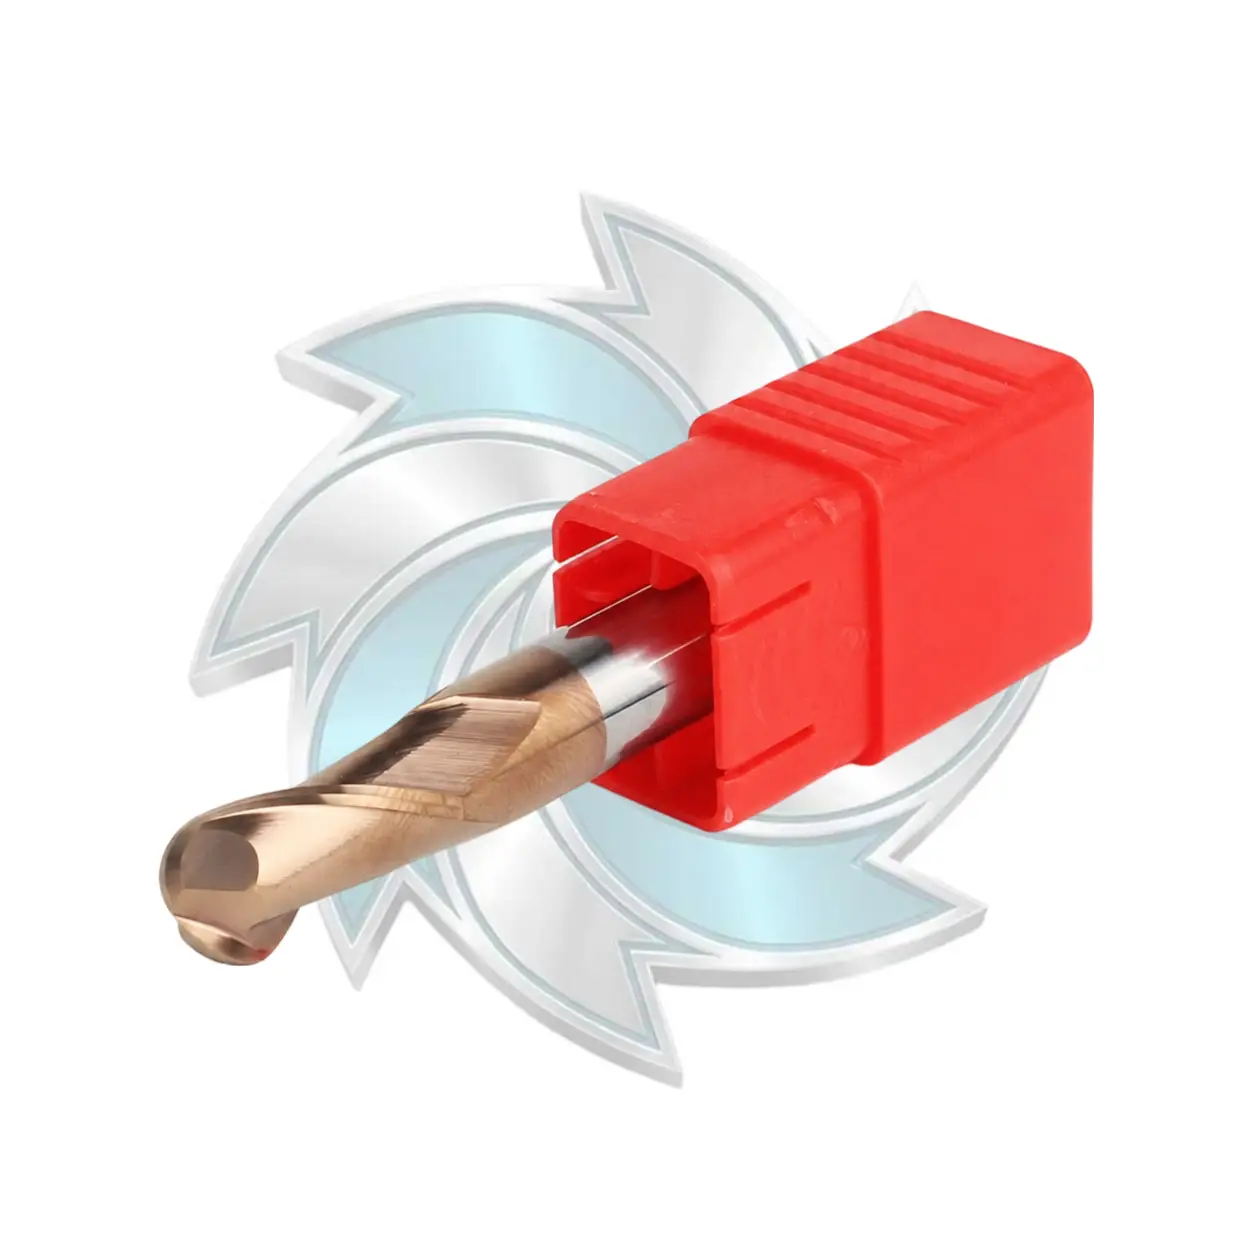
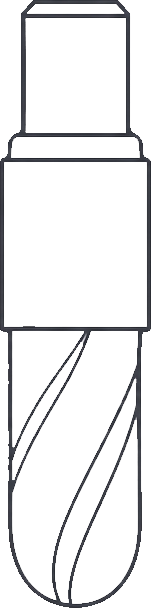
Engineered by Durable Mills, the HRC55 2 Flute Ball Nose End Mill is a high-performance, economical universal solid carbide milling solution developed specifically for precise 3D contouring, copy milling, and finish machining. Manufactured with 10% cobalt sub-micrograin carbide substrate (HRA 91.2–91.7), it strikes the optimal balance between edge toughness and wear resistance when cutting workpieces up to 55 HRC.
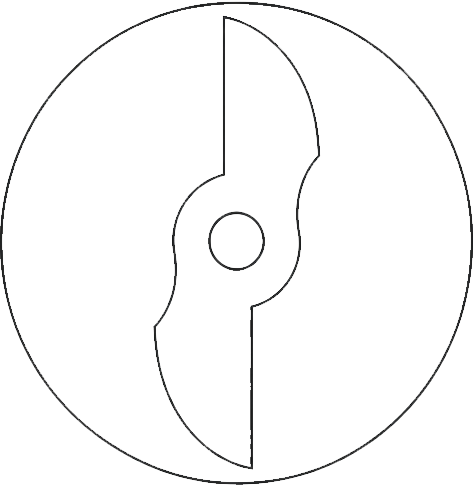
The optimized 2-blade profile geometry significantly outperforms traditional 4-flute cutters in profile accuracy and chip evacuation, eliminating chatter marks and providing mirror-like surface finishes across die and mold components.
| Workpiece Material | Cutting Depth (ap) | Cutting Width (ae) | Cutting Speed (Vc) | Feed Per Tooth (fz) |
|---|---|---|---|---|
| Carbon Steel / Alloy Steel (<35 HRC) | ap ≤ 0.2D | ae ≤ 0.3D | 170 m/min | 0.008D mm/z |
| Alloy Steel (35–48 HRC) | ap ≤ 0.15D | ae ≤ 0.2D | 120–150 m/min | 0.006D mm/z |
| Stainless Steel | ap ≤ 0.15D | ae ≤ 0.2D | 100–130 m/min | 0.005D mm/z |
| Gray Cast Iron / Ductile Iron (<32 HRC) | ap ≤ 0.2D | ae ≤ 0.2D | 150 m/min | 0.0065D mm/z |
| Hardened Steel (45–55 HRC) | ap ≤ 0.1D | ae ≤ 0.15D | 80–110 m/min | 0.004D mm/z |
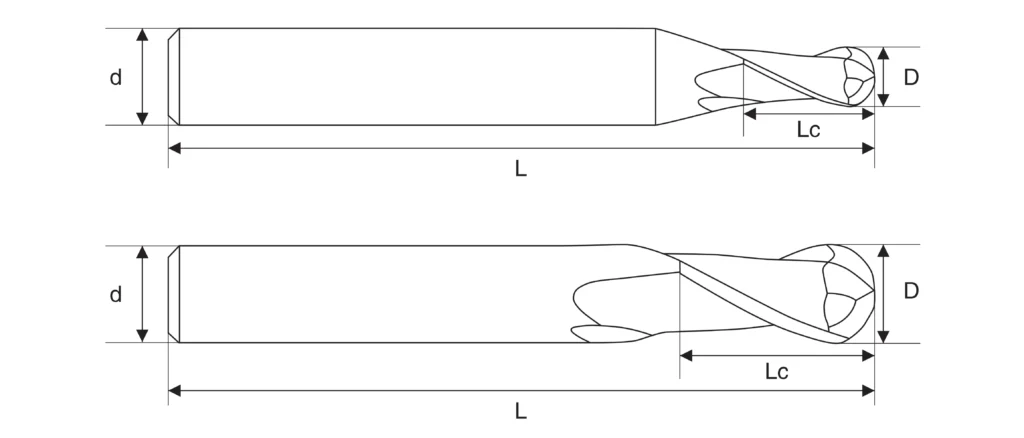
| Model / Type | Radius R (mm) | Flute Length Lc (mm) | Shank Dia. d (mm) | Overall Length L (mm) | Flutes |
|---|---|---|---|---|---|
| DM-R1.5*6*3*50*2T | 1.5 | 6 | 3 | 50 | 2 |
| DM-R1.5*6*3*75*2T | 1.5 | 6 | 3 | 75 | 2 |
| DM-R1.5*6*3*100*2T | 1.5 | 6 | 3 | 100 | 2 |
| DM-R0.5*2*4*50*2T | 0.5 | 2 | 4 | 50 | 2 |
| DM-R0.75*3*4*50*2T | 0.75 | 3 | 4 | 50 | 2 |
| DM-R1*4*4*50*2T | 1.0 | 4 | 4 | 50 | 2 |
| DM-R1.25*5*4*50*2T | 1.25 | 5 | 4 | 50 | 2 |
| DM-R1.5*6*4*50*2T | 1.5 | 6 | 4 | 50 | 2 |
| DM-R1.75*7*4*50*2T | 1.75 | 7 | 4 | 50 | 2 |
| DM-R2*8*4*50*2T | 2.0 | 8 | 4 | 50 | 2 |
| DM-R2*8*4*75*2T | 2.0 | 8 | 4 | 75 | 2 |
| DM-R2*8*4*100*2T | 2.0 | 8 | 4 | 100 | 2 |
| DM-R0.5*2*4*75*2T | 0.5 | 2 | 4 | 75 | 2 |
| DM-R0.75*3*4*75*2T | 0.75 | 3 | 4 | 75 | 2 |
| DM-R1*4*4*75*2T | 1.0 | 4 | 4 | 75 | 2 |
| DM-R1.25*5*4*75*2T | 1.25 | 5 | 4 | 75 | 2 |
| DM-R1.5*6*4*75*2T | 1.5 | 6 | 4 | 75 | 2 |
| DM-R2.5*10*5*50*2T | 2.5 | 10 | 5 | 50 | 2 |
| DM-R2.5*10*5*75*2T | 2.5 | 10 | 5 | 75 | 2 |
| DM-R2.5*10*5*100*2T | 2.5 | 10 | 5 | 100 | 2 |
| DM-R2.5*10*6*50*2T | 2.5 | 10 | 6 | 50 | 2 |
| DM-R0.5*2*6*50*2T | 0.5 | 2 | 6 | 50 | 2 |
| DM-R0.75*3*6*50*2T | 0.75 | 3 | 6 | 50 | 2 |
| DM-R1*4*6*50*2T | 1.0 | 4 | 6 | 50 | 2 |
| DM-R1.25*5*6*50*2T | 1.25 | 5 | 6 | 50 | 2 |
| DM-R1.5*6*6*50*2T | 1.5 | 6 | 6 | 50 | 2 |
| DM-R1.75*7*6*50*2T | 1.75 | 7 | 6 | 50 | 2 |
| DM-R2*8*6*50*2T | 2.0 | 8 | 6 | 50 | 2 |
| DM-R2.5*10*6*50*2T | 2.5 | 10 | 6 | 50 | 2 |
| DM-R3*12*6*50*2T | 3.0 | 12 | 6 | 50 | 2 |
| DM-R3*12*6*75*2T | 3.0 | 12 | 6 | 75 | 2 |
| DM-R3*12*6*100*2T | 3.0 | 12 | 6 | 100 | 2 |
| DM-R3*12*6*150*2T | 3.0 | 12 | 6 | 150 | 2 |
| DM-R3.5*14*8*60*2T | 3.5 | 14 | 8 | 60 | 2 |
| DM-R4*16*8*60*2T | 4.0 | 16 | 8 | 60 | 2 |
| DM-R4*16*8*75*2T | 4.0 | 16 | 8 | 75 | 2 |
A 2-flute ball nose cutter provides wider flute gullets for optimal chip evacuation and minimizes tool deflection during complex 3D profiling. This gives superior contour accuracy and prevents thermal re-cutting on pre-hardened steels.
Yes, our high-temperature composite coating supports dry high-speed milling with an air blow. However, applying mist or flood coolant is recommended when milling stainless steels to improve surface finish and maximize tool life.
This series is optimized for workpieces under 55 HRC, such as P20, 718, NAK80, carbon steels, and ductile iron. For steels harder than 58 HRC, we recommend selecting our HRC65 specialized series.
Yes, as a dedicated cutting tool manufacturer, we provide OEM laser-marking, custom flute geometries, and wholesale volume pricing. Please submit your inquiry through our Contact Page or reach our engineering sales team directly at info@durablemills.com.