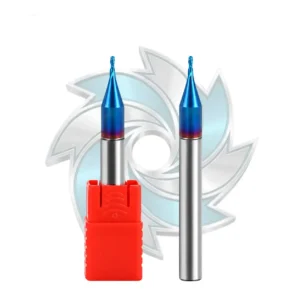
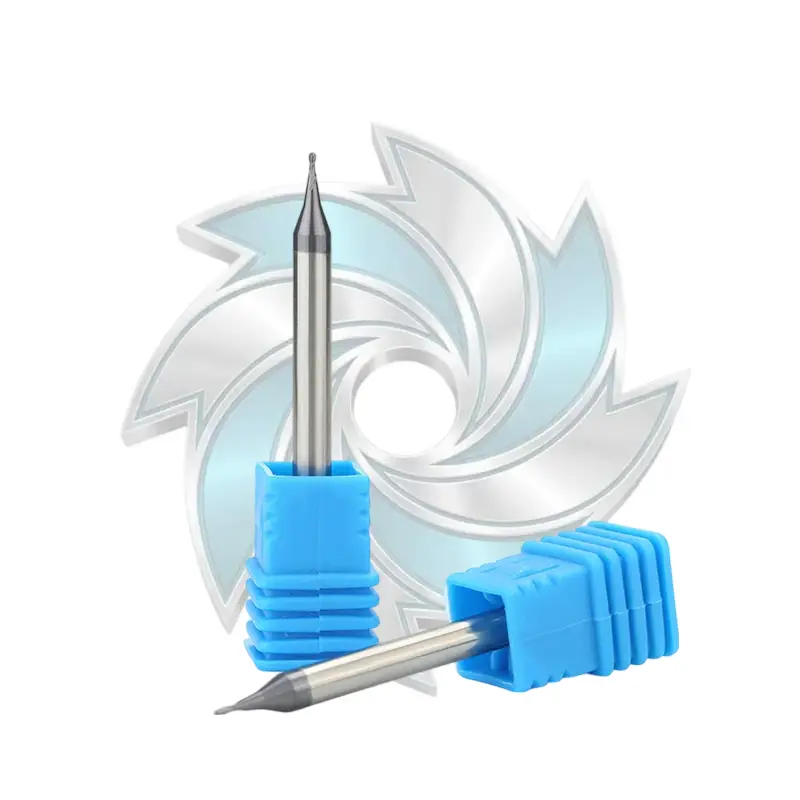
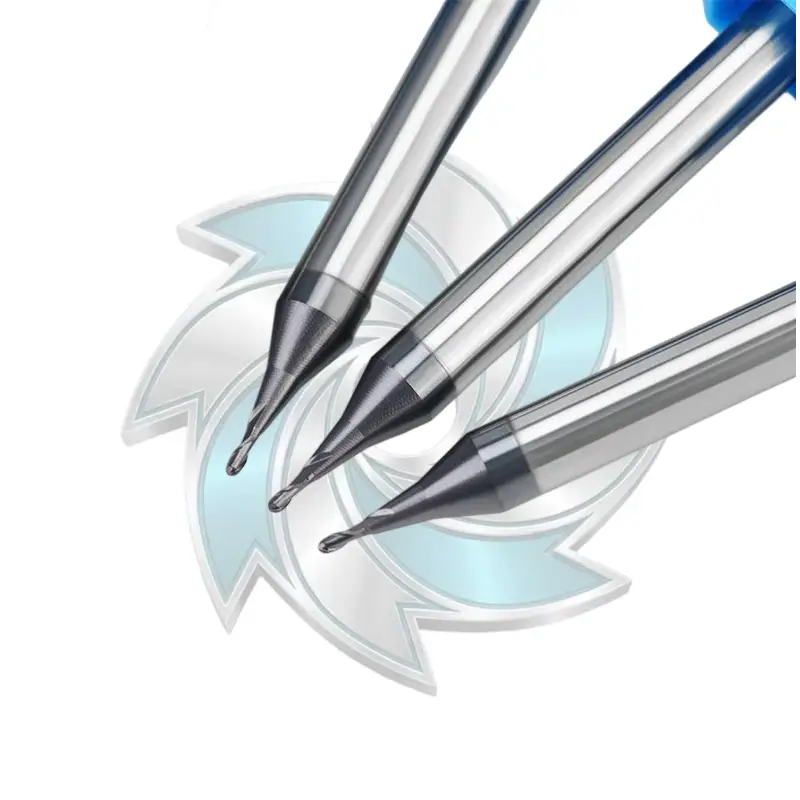
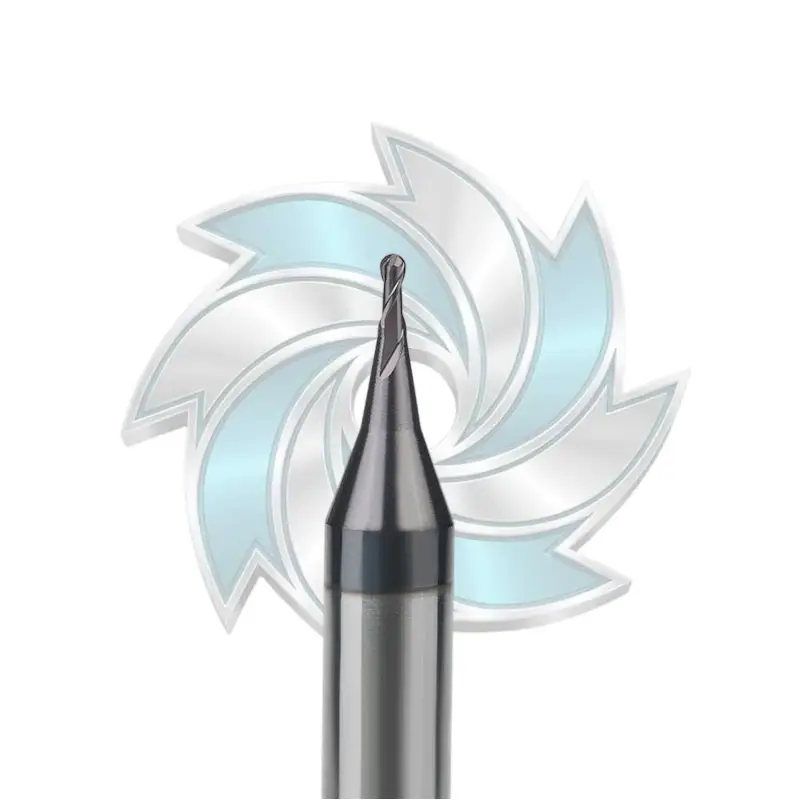
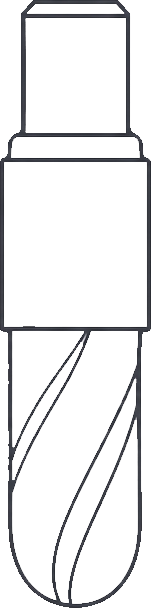
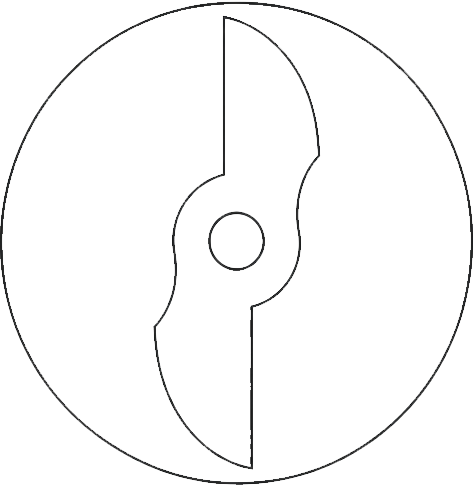
Manufactured by Durable Mills, our HRC60 2-flute miniature ball end mill lineup is engineered specifically for intricate 3D profiling, precision die and mold cavities, and micro-contouring applications. Constructed from ultra-fine 0.4 μm grain solid carbide with an AlTiN nano-coating, these miniature tools deliver outstanding cutting edge rigidity, exceptional thermal stability, and prolonged tool life across tough and hardened workpieces.

| Model | Radius (R / mm) | Flute Length (Lc / mm) | Shank Dia. (d / mm) | Overall Length (L / mm) | Flutes |
|---|---|---|---|---|---|
| DM-R0.1*0.4*4*50 | 0.1 | 0.4 | 4.0 | 50 | 2 |
| DM-R0.15*0.6*4*50 | 0.15 | 0.6 | 4.0 | 50 | 2 |
| DM-R0.2*0.8*4*50 | 0.2 | 0.8 | 4.0 | 50 | 2 |
| DM-R0.25*1*4*50 | 0.25 | 1.0 | 4.0 | 50 | 2 |
| DM-R0.3*1.2*4*50 | 0.3 | 1.2 | 4.0 | 50 | 2 |
| DM-R0.35*1.4*4*50 | 0.35 | 1.4 | 4.0 | 50 | 2 |
| DM-R0.4*1.6*4*50 | 0.4 | 1.6 | 4.0 | 50 | 2 |
| DM-R0.45*1.8*4*50 | 0.45 | 1.8 | 4.0 | 50 | 2 |
| Workpiece Material | Depth of Cut (ap) | Cutting Width (ae) | Linear Speed (vc) | Feed Rate (fz) |
|---|---|---|---|---|
| Carbon Steel, Alloy Steel (<35 HRC) | ap ≤ 1.5D | ae ≤ 0.15D | 170 m/min | 0.008D mm/z |
| Alloy Steel (35–48 HRC) | ap ≤ 1.2D | ae ≤ 0.12D | 130–150 m/min | 0.007D mm/z |
| Stainless Steels (Martensitic/Austenitic) | ap ≤ 1.0D | ae ≤ 0.10D | 110–130 m/min | 0.006D mm/z |
| Gray Cast Iron, Ductile Iron (<32 HRC) | ap ≤ 1.5D | ae ≤ 0.15D | 150 m/min | 0.0065D mm/z |
| Alloy Steel, Hardened Steel (45–65 HRC) | ap ≤ 0.8D | ae ≤ 0.08D | 80–120 m/min | 0.005D mm/z |
*Please adjust parameters according to machine tool rigidity, holder balance, and specific workpiece clamping conditions.
For micro radii below R0.5mm, spindle runout must be kept within 0.003 mm (TIR). Excessive runout can cause uneven flute loading and premature edge chipping.
Yes. Durable Mills offers comprehensive OEM/ODM solutions, including custom neck relief, specialized shank diameters, and white-label packaging for industrial distributors.
High-pressure air blast or micro-lubrication (MQL oil mist) is strongly recommended over standard water-soluble flood coolant to avoid thermal fatigue and thermal cracking on submicron carbide edges.
You can submit an inquiry directly through our Contact Page or send your tool list to our sales department at info@durablemills.com for an immediate quotation.