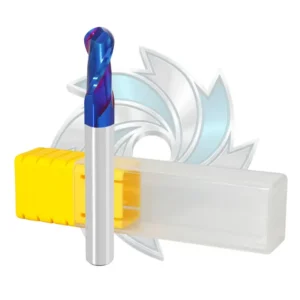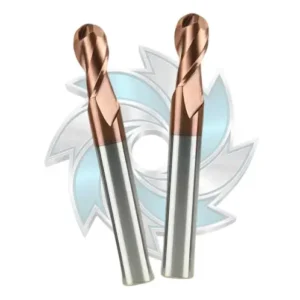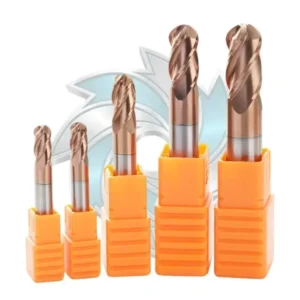
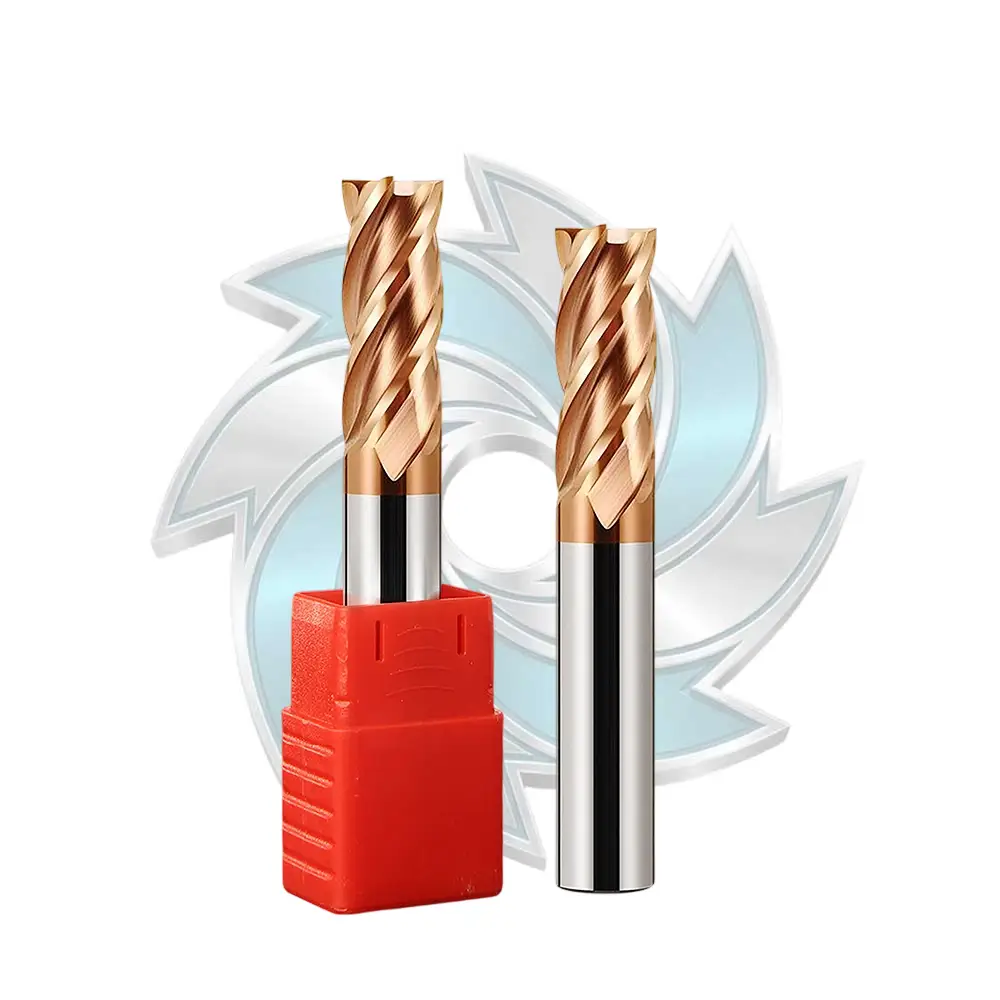
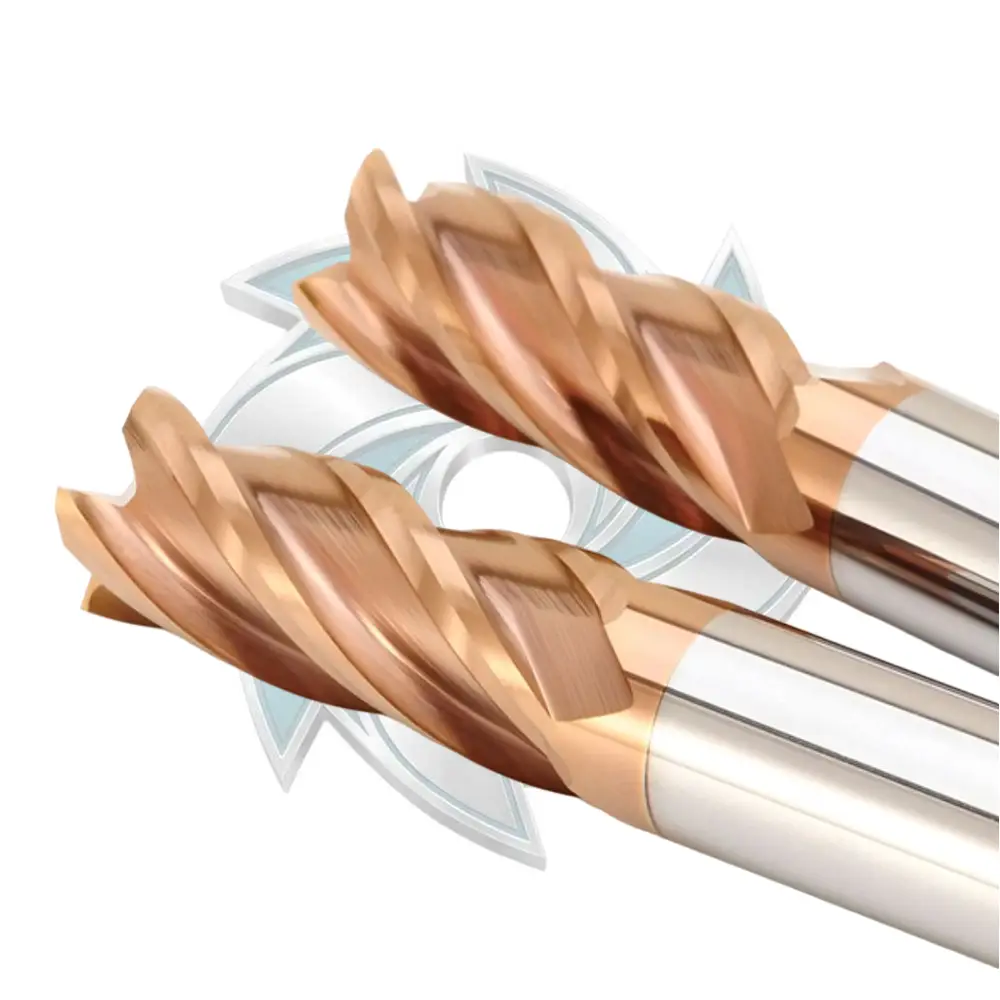
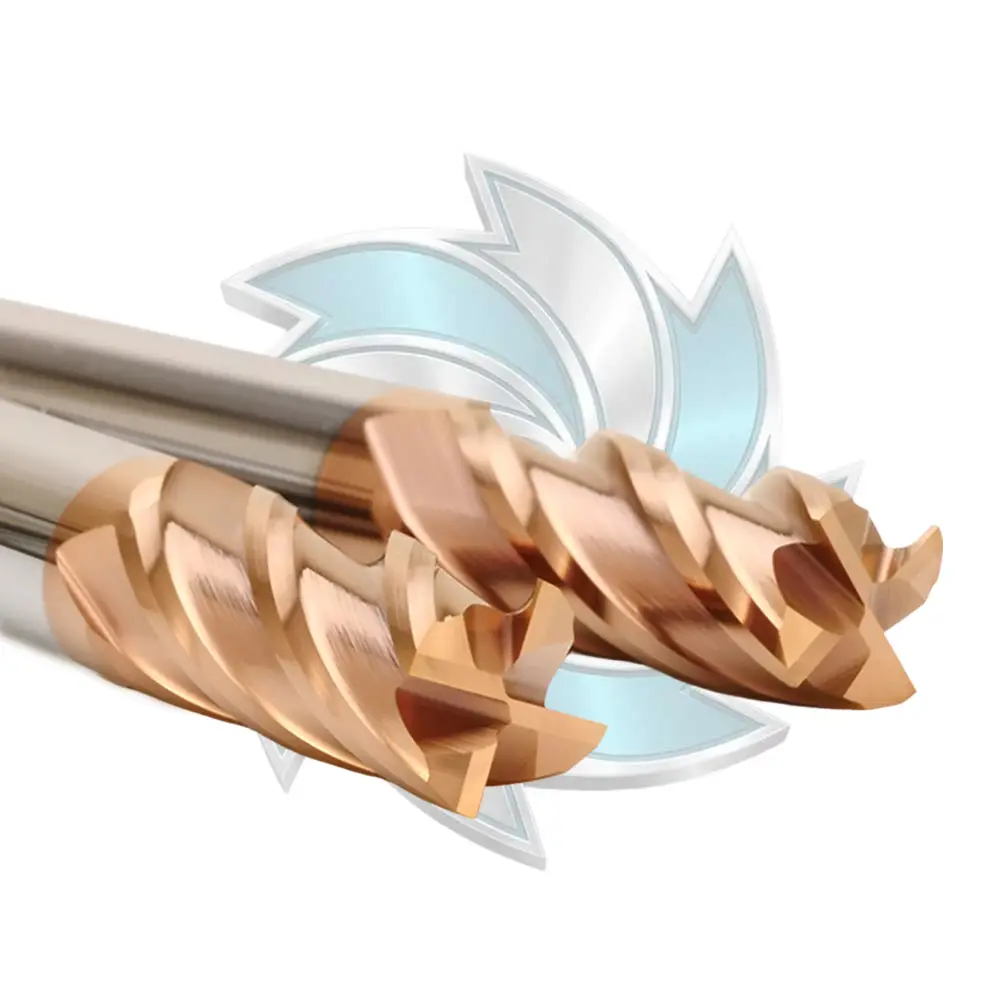
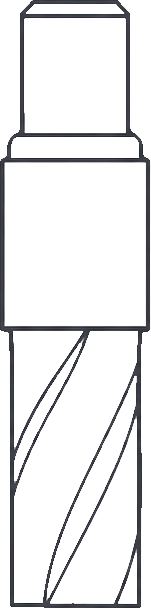
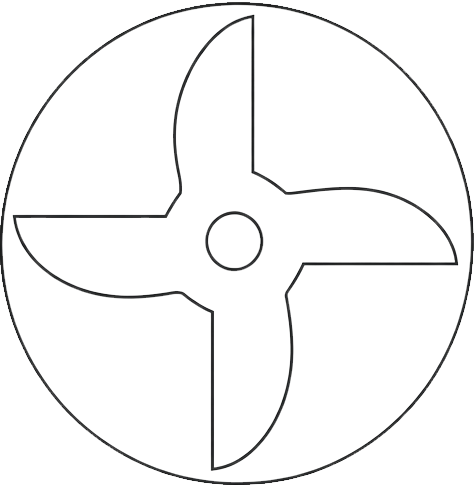
Manufactured by Durable Mills, this premium industrial HRC68 4 Flute End Mill is designed specifically for aggressive high-speed milling and finish profiling of hardened steels and chilled cast iron up to HRC68. Combining an advanced nano-composite coating with an ultra-fine carbide substrate, our 4 flute flat end milling cutter provides extreme thermal stability and wear resistance under intense mold and die cutting conditions.
| Property | Value Range / Specification |
|---|---|
| Cobalt Content (Co) | 9% – 10% |
| Carbide Grain Size | 0.3 – 0.8 μm (Ultra-Fine Micrograin) |
| Substrate Hardness | HRA 91.5 – 94 (Machining capability up to HRC 68) |
| End Geometry | Flat / Square End with Negative Rake Cutting Edge |
| Workpiece Material | Axial Depth (ap) | Radial Width (ae) | Cutting Speed (vc) | Feed per Tooth (fz) |
|---|---|---|---|---|
| Carbon Steel & Alloy Steel (<35 HRC) | Standard | Standard | Adjust per setup | Adjust per setup |
| Alloy Steel (35 – 48 HRC) | Standard | Standard | Adjust per setup | Adjust per setup |
| Stainless Steels | Standard | Standard | Adjust per setup | Adjust per setup |
| Gray Cast Iron & Ductile Cast Iron (<32 HRC) | Standard | Standard | Adjust per setup | Adjust per setup |
| Aluminum Alloy & Copper Alloy | Compatible | Compatible | Adjust per setup | Adjust per setup |
| Hardened Steel & Alloy Steel (45 – 65+ HRC) | ≤ 1.5D | ≤ 0.02D | 70 – 100 m/min | 0.007D mm/z |

| Model No. | Cutting Dia (D) mm | Flute Length (Lc) mm | Shank Dia (d) mm | Overall Length (L) mm | Flutes |
|---|---|---|---|---|---|
| DM-3*8*3*50*4T | 3 | 8 | 3 | 50 | 4 |
| DM-3*12*3*75*4T | 3 | 12 | 3 | 75 | 4 |
| DM-3*15*3*100*4T | 3 | 15 | 3 | 100 | 4 |
| DM-1*3*4*50*4T | 1 | 3 | 4 | 50 | 4 |
| DM-1.5*4*4*50*4T | 1.5 | 4 | 4 | 50 | 4 |
| DM-2*5*4*50*4T | 2 | 5 | 4 | 50 | 4 |
| DM-2.5*7*4*50*4T | 2.5 | 7 | 4 | 50 | 4 |
| DM-3*8*4*50*4T | 3 | 8 | 4 | 50 | 4 |
| DM-3.5*10*4*50*4T | 3.5 | 10 | 4 | 50 | 4 |
| DM-4*10*4*50*4T | 4 | 10 | 4 | 50 | 4 |
| DM-4*16*4*75*4T | 4 | 16 | 4 | 75 | 4 |
| DM-4*20*4*100*4T | 4 | 20 | 4 | 100 | 4 |
| DM-5*13*5*50*4T | 5 | 13 | 5 | 50 | 4 |
| DM-5*20*5*75*4T | 5 | 20 | 5 | 75 | 4 |
| DM-5*25*5*100*4T | 5 | 25 | 5 | 100 | 4 |
| DM-1*3*6*50*4T | 1 | 3 | 6 | 50 | 4 |
| DM-1.5*4*6*50*4T | 1.5 | 4 | 6 | 50 | 4 |
| DM-2*5*6*50*4T | 2 | 5 | 6 | 50 | 4 |
| DM-2.5*7*6*50*4T | 2.5 | 7 | 6 | 50 | 4 |
| DM-3*8*6*50*4T | 3 | 8 | 6 | 50 | 4 |
| DM-3.5*10*6*50*4T | 3.5 | 10 | 6 | 50 | 4 |
| DM-4*10*6*50*4T | 4 | 10 | 6 | 50 | 4 |
| DM-4.5*12*6*50*4T | 4.5 | 12 | 6 | 50 | 4 |
| DM-5*13*6*50*4T | 5 | 13 | 6 | 50 | 4 |
| DM-6*15*6*50*4T | 6 | 15 | 6 | 50 | 4 |
| DM-6*25*6*75*4T | 6 | 25 | 6 | 75 | 4 |
| DM-6*30*6*100*4T | 6 | 30 | 6 | 100 | 4 |
| DM-6*40*6*150*4T | 6 | 40 | 6 | 150 | 4 |
| DM-7*18*8*60*4T | 7 | 18 | 8 | 60 | 4 |
| DM-8*20*8*60*4T | 8 | 20 | 8 | 60 | 4 |
| DM-8*28*8*75*4T | 8 | 28 | 8 | 75 | 4 |
| DM-8*35*8*100*4T | 8 | 35 | 8 | 100 | 4 |
| DM-8*50*8*150*4T | 8 | 50 | 8 | 150 | 4 |
| DM-9*23*10*75*4T | 9 | 23 | 10 | 75 | 4 |
| DM-10*25*10*75*4T | 10 | 25 | 10 | 75 | 4 |
| DM-10*40*10*100*4T | 10 | 40 | 10 | 100 | 4 |
This series is specifically engineered for quenched and hardened steels (HRC 45-68), die mold steels (such as SKD11, SKD61, D2), high-speed steels, and chilled cast irons, while remaining capable of handling standard alloy steels and stainless steels.
Machining hardened metals creates tremendous edge stress. A negative rake angle adds physical support behind the cutting edge, drastically reducing cutting vibration and preventing edge chipping under heavy CNC loads.
Yes. Durable Mills supports wholesale distributors and machining facilities with custom shank lengths, tailored coatings, and laser-etched OEM branding. Inquire directly through our Contact Page or email info@durablemills.com.
For milling steel above HRC 60, dry machining with high-pressure air blast or oil mist (MQL) is highly recommended. This prevents thermal shock cracking on the micrograin carbide cutting edge.
Looking for Reliable Carbide Cutting Tool Solutions?
Contact our technical sales team for wholesale pricing, bulk volume orders, or custom tool consultations.