If you have ever spent a shift running aluminum billets through a high-speed CNC mill, you know that soft metals can cause surprisingly hard headaches. Aluminum alloys like 6061-T6, 7075-T6, and cast A380 look easy to cut on paper. However, the moment your spindle hits high RPMs, that ductile, gummy material loves nothing more than sticking to your tool flutes, galling along the margins, and throwing your hole locations out of spec.
Too many machine shops treat tooling procurement for spot drilling as an afterthought. An operator or buyer grabs an off-the-shelf 90-degree steel spotter or a generic jobber bit from the tool crib, pops it into an ER collet, and wonders why the downstream drill wanders or snaps after fifty cycles. Choosing a purpose-built carbide spot drill for aluminum is not an optional upgrade—it is positional insurance for your entire holemaking sequence.
Whether you run a high-mix job shop or high-volume automotive production, understanding point geometry, web thinning, and flute micro-polishing helps you source the right tools from an experienced spot drill manufacturer. When you balance the correct tool parameters, you stop fighting bird nesting, eliminate secondary deburring steps, and keep your cycle times fast.
Standard spotting tools are usually ground with geometry suited for carbon steels, alloy steels, or general cast iron. In those harder materials, high cutting pressure breaks chips into manageable fragments. Aluminum does not play by those rules.
When cutting non-ferrous alloys, the material undergoes severe plastic deformation before it shears. Heat and intense localized pressure at the cutting lip quickly cause aluminum molecules to cold-weld directly onto the carbide surface. In metal cutting science, this is known as built-up edge (BUE), a condition thoroughly studied across manufacturing engineering because it ruins tool geometry and workpiece surface integrity.
Shop Floor Insight: When aluminum welds to your tool’s chisel edge, the tool stops cutting and starts plowing. The axial thrust forces spike instantly, pushing the tool sideways along the path of least resistance. That is how your true position gets blown before your secondary drill even touches the part.
The consequences of using an improper spotting tool in aluminum follow a predictable chain reaction:
Investing in a dedicated carbide spot drill for aluminum prevents these failures right at the start of your cycle.
One of the first things to look at when evaluating a carbide spot drill for aluminum is the surface finish inside the flute. If you can see prominent grinding lay lines or feel ridges when sliding a fingernail along the flute throat, that tool will pack with chips in 6061-T6.
Industrial surface roughness standards, such as ISO 21920 for profile roughness evaluation, measure the arithmetical mean deviation of the roughness profile (Ra). For steel machining, a standard ground flute with an Ra between 0.40 µm and 0.60 µm is standard practice. For aluminum, that surface is far too coarse.
Flute Surface Comparison:
- Standard Ground Flute (Ra 0.40 – 0.60 µm): Microscopic grinding ridges grip ductile aluminum chips, leading to micro-welding, heat buildup, and flute packing within 100 to 200 cycles.
- Fine Ground Flute (Ra 0.20 – 0.35 µm): Moderate chip evacuation; works acceptably in free-machining brass or cast alloys, but struggles with continuous stringy chips in wrought aluminum.
- Mirror Polished Flute (Ra < 0.08 – 0.10 µm): Ultra-smooth, slick surface creates near-zero friction. Chips glide effortlessly up the flutes and eject cleanly without welding to the carbide substrate.
When you purchase a mirror-polished carbide spot drill for aluminum, that ultra-smooth flute acts almost like a non-stick coating. It allows the cut chip to curl naturally and fling away under centrifugal force, even when run with modest flood coolant pressures or through MQL (Minimum Quantity Lubrication) systems.
Take a look at the mirror-ground gullets on our flagship carbide spot drill for aluminum to see how optical-grade finishing prevents chip pack and lowers cycle friction.
A widespread habit among CNC programmers is calling up a 90-degree spotter for every single hole cycle. The logic seems clear enough: a 90-degree tool leaves a neat 45-degree lead-in chamfer for a threaded tap while spotting the hole at the same time, saving a tool pocket in the carousel.
However, if your primary holemaking tool is a modern high-performance carbide drill with a 135-degree or 140-degree point angle, spotting with a 90-degree tool is a bad combination.
When a drill with a 140° point enters a conical 90° spot hole, the drill’s sharp outer corners make contact with the steep walls of the chamfer first. The self-centering web of the drill is suspended in mid-air, completely unsupported.
Because the entire rotational cutting load hits the fragile outer margins before the center stabilizes, the corners experience heavy vibration and chipping. The drill chatters, wanders, and loses its cutting margin prematurely.
When you pair a 142° carbide spot drill for aluminum with a 140° secondary drill, the geometry works in your favor:
| Spotting Point Angle | Ideal Downstream Tooling | Primary Machining Advantage | Common Trade-off |
|---|---|---|---|
| 90° Spot Drill | 60° – 90° Points, Thread Taps, Reamers | Spots and deburrs/chamfers in a single cycle | Chips outer corners of 135° to 140° solid carbide drills |
| 120° Spot Drill | 118° HSS & Cobalt Twist Drills | Matches traditional drill geometry; prevents corner bite | Not flat enough for high-penetration 140° carbide drills |
| 142° Spot Drill | 135° – 140° High-Performance Carbide Drills | Centers the drill web first; eliminates shock and walk | Cannot produce a finished 45° chamfer in the same stroke |
To find the right mix of profiles for your production cell, review the options in our spotting & center drills category.


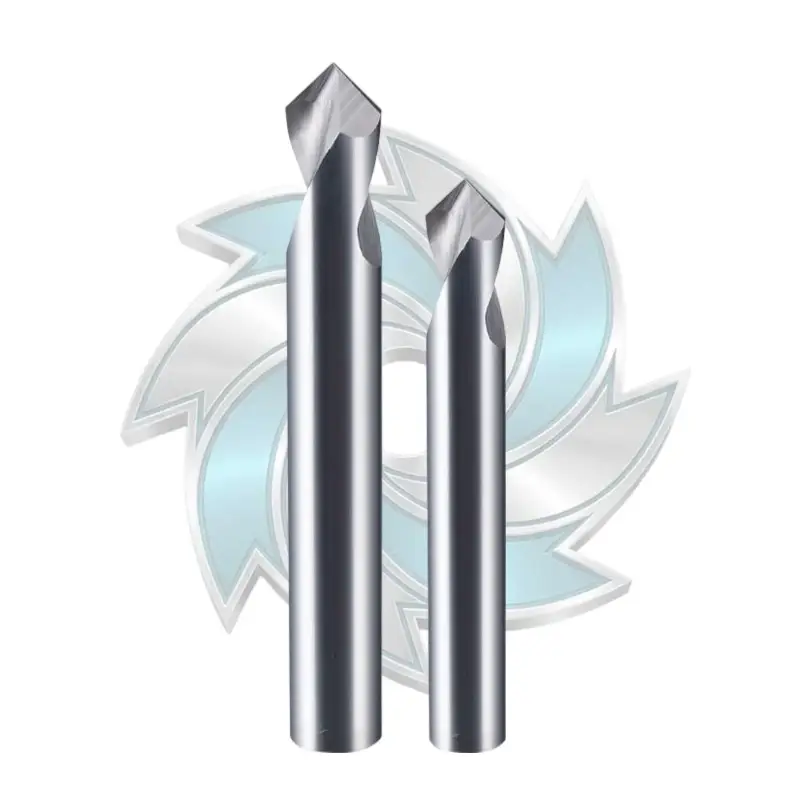
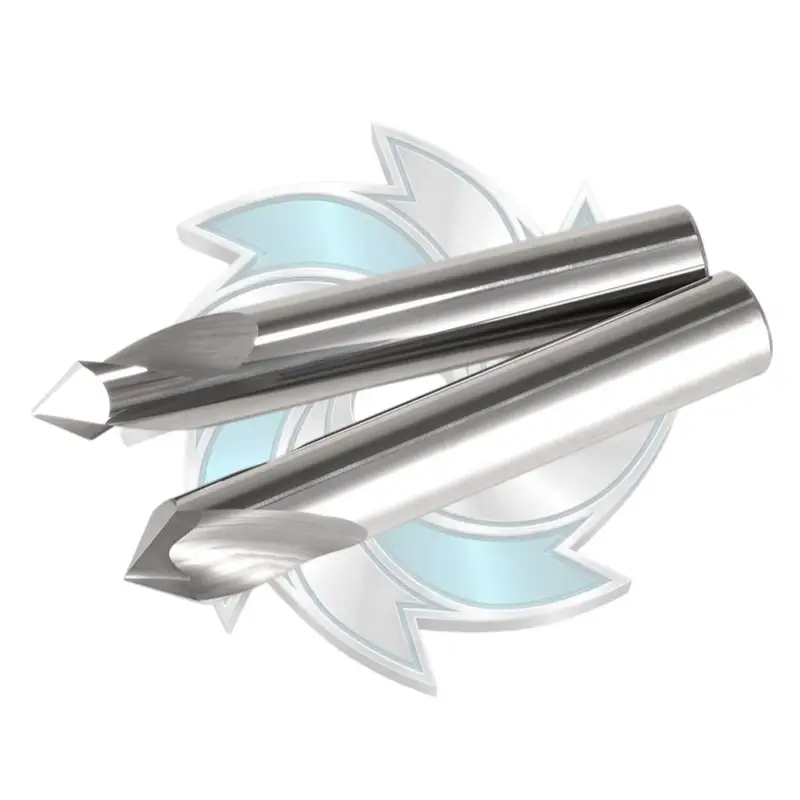
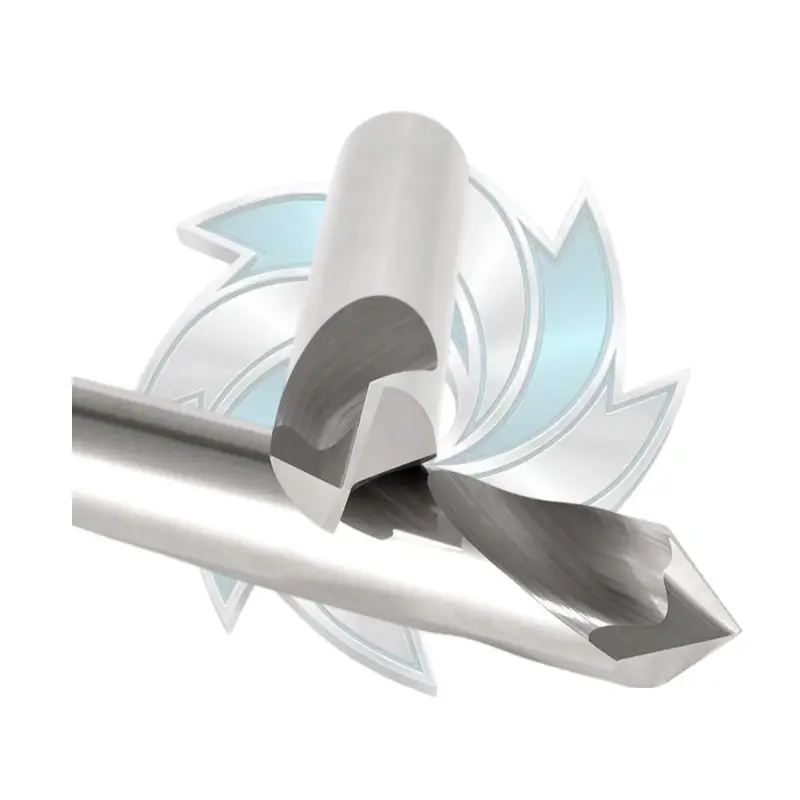
Our high-precision carbide spot drill for aluminum delivers reliable centering accuracy and clean 90-degree chamfering in non-ferrous machining. Manufactured from premium micrograin tungsten carbide, this carbide spot drill for aluminum effectively prevents drill wander and extends subsequent tool life. Upgrade your CNC manufacturing efficiency with high-performance spotting drills from Durable Mills.
Do not let your CNC operators guess spot drill depth at the machine offset screen. Leaving an undersized spot means the secondary drill gains no guidance, while an oversized spot slows down cycle times and wastes tool life.
You can calculate the exact target depth using this straightforward formula:
Target Depth = (Finished Hole or Chamfer Diameter / 2) / tan(Spot Tool Point Angle / 2)
Let us look at two practical shop examples:
Because the tool angle is 90 degrees, the half-angle is 45 degrees, and the tangent of 45 degrees equals 1.0:
Because the tool angle is 142 degrees, the half-angle is 71 degrees, and the tangent of 71 degrees equals roughly 2.9042:
Notice how much shallower the 142° spot is compared to the 90° tool. The flatter angle provides full centering support for the secondary drill’s chisel edge with less Z-axis travel, cutting precious seconds off every hole cycle across high-volume runs.
A reliable carbide spot drill for aluminum is defined by more than just its point angle. Every surface from the chisel edge to the shank tolerance directly impacts tool rigidity, cutting temperatures, and hole location accuracy.
Standard twist drill blanks have a thick central web to resist twisting forces. But that thick web leaves a flat, blunt chisel edge right at the tool center. In aluminum, this blunt section does not cut; it rubs, squashes, and deforms the stock.
A precision carbide spot drill for aluminum incorporates web thinning, often referred to as a split point or notched web. By grinding away material at the chisel center, the non-cutting flat is reduced to a microscopic point. The tool starts cutting the instant it touches the billet, reducing axial thrust force by up to 40% according to machining data published by ASM International.
Because aluminum is ductile and springs back slightly behind the cutting edge, tooling requires generous relief angles:
Without this relief, the heel of the cutting lip rubs against the conical walls of the hole. That rubbing generates friction heat, leading to premature tool wear and localized thermal expansion of your workpiece.
Long flutes are necessary for deep-hole drilling, but they work against you when spotting. Any unnecessary flute length increases tool overhang and flexibility under load.
A high-performance aluminum spotting drill keeps flutes stubby, maintaining a flute length-to-diameter ratio (L/D) between 1.5:1 and 2.0:1. The thick solid carbide core behind the cutting zone resists bending moments, keeping tool deflection to a minimum when entering uneven cast skins or angled surfaces.
Even the best point geometry will not help if your tool shank runs out in the toolholder. Premium CNC aluminum tools are ground to an h6 shank tolerance, guaranteeing roundness and straightness. Combined with a balanced toolholder, your Total Indicator Runout (TIR) should stay below 0.003 mm (0.00012 inches).
Choosing the right grade of tungsten carbide is a balancing act between hardness and edge strength. Some machine shops mistakenly order ultra-hard micrograin carbide with low cobalt binder, assuming higher hardness automatically means longer tool life.
However, aluminum machining—especially when drilling cast aluminum blocks with abrasive silicon content (like A356 or A380)—requires high impact resistance. Interrupted cuts and surface scale can cause micro-chipping on brittle cutting edges.
Recommended Carbide Specifications for Aluminum Spotting:
- Substrate Grain Size: 0.6 µm to 0.8 µm (sub-micron grain structure)
- Cobalt Binder Content: 10% to 12% by weight
- Transverse Rupture Strength (TRS): 3,800 to 4,200 MPa
- Hardness Rating: 91.8 to 92.6 HRA
This metallurgical composition gives your carbide spot drill for aluminum the fracture toughness needed to handle rapid plunge cycles and surface scale without chipping, while retaining a razor-sharp cutting edge for tens of thousands of holes.
Tool manufacturers structure and document tool classification, physical properties, and dimensions using ISO 13399, the international standard for cutting tool data representation. Adhering to these standards ensures your digital tooling library matches physical shop performance down to the micron.
To understand how flute polish and point angle impact daily operations, consider this machining comparison from a production line producing hydraulic aerospace manifolds.
The shop tested an inexpensive general-purpose 90° uncoated spotter against a Durable Mills 142° mirror-polished carbide spot drill for aluminum.
| Production Metric | Standard 90° General-Purpose Spotter | Durable Mills 142° Mirror-Polished Spotter | Shop Floor Impact |
|---|---|---|---|
| Spindle Speed | 5,500 RPM | 11,500 RPM | Cycle time cut by 52% |
| Plunge Feed Rate | 18 IPM (0.45 m/min) | 48 IPM (1.22 m/min) | Significantly faster hole-to-hole moves |
| Flute Condition at 2,000 Holes | Visible chip galling; aluminum packing in gullet | Clean, mirror-bright surface; no chip adherence | Eliminated mid-shift operator cleaning stops |
| Hole Entrance Burr | Heavy roll-over burr; required manual deburring | Razor-clean entrance; zero deburring needed | Saved 4.5 minutes of post-machining labor per part |
| Downstream Drill Life | 2 drill breakages per 10,000 holes | 0 drill breakages per 10,000 holes | Saved tooling costs and prevented scrapped parts |
| Hole True Position (CMM) | 0.038 mm (borderline tolerance) | 0.008 mm (well within tolerance) | 100% CMM pass rate on first-article inspections |
By matching the 142-degree spotting angle to the 140-degree twist drill and using mirror-polished flutes, the shop eliminated tool breakage, prevented entry burrs, and recovered valuable machining hours every week.


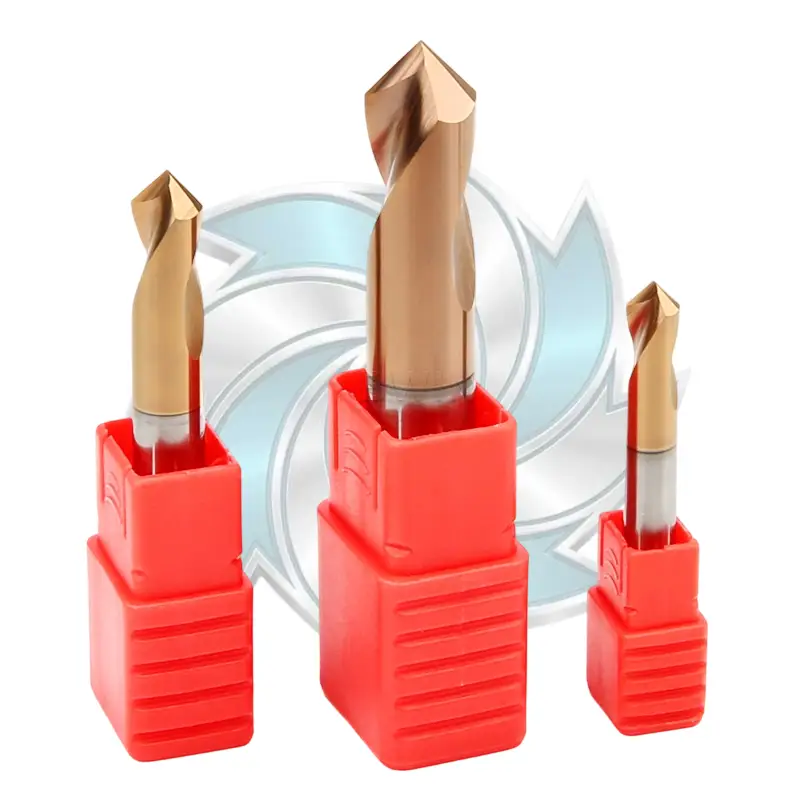
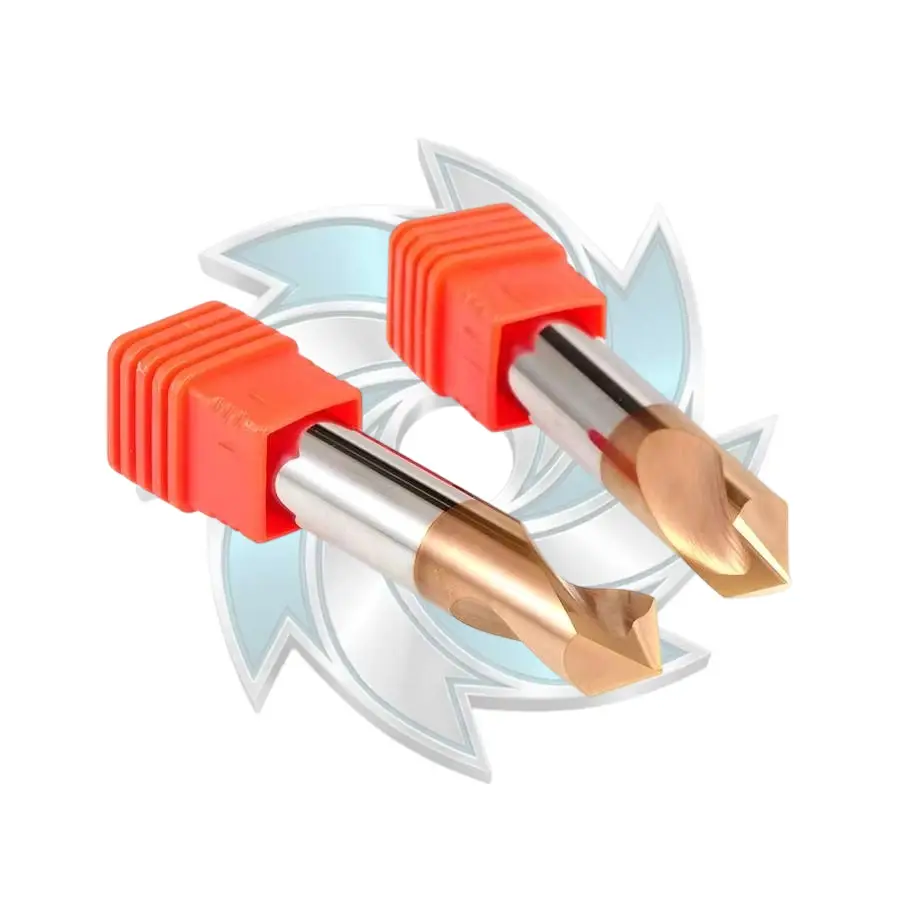
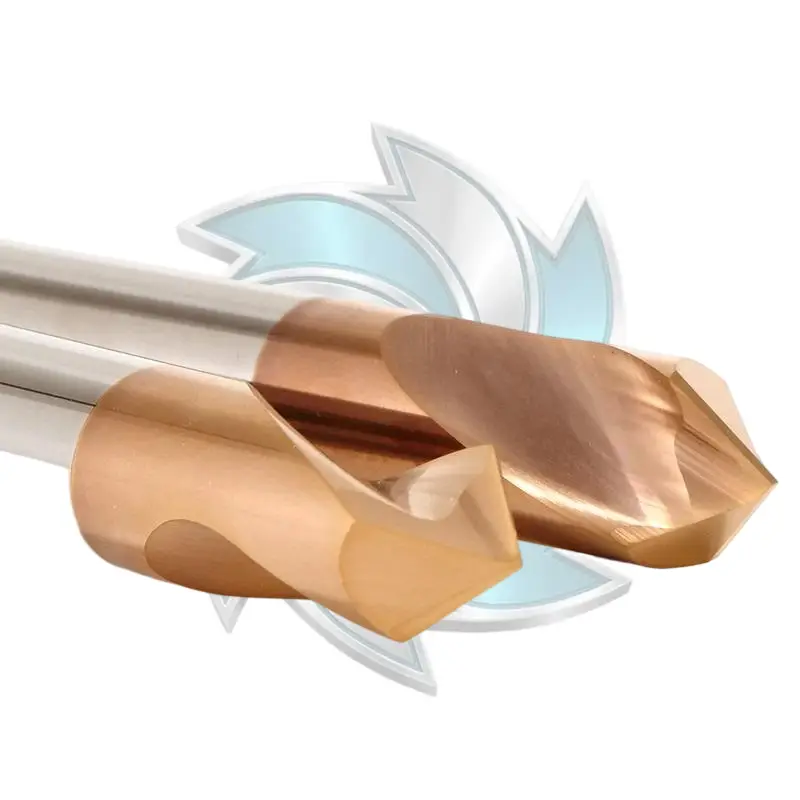
The Solid Carbide Spot Drill delivers exceptional centering accuracy and chamfering efficiency for steels up to HRC55. Engineered for rigid CNC setups, this solid carbide spot drill eliminates tool deflection. Durable Mills manufactures high-durability carbide spot drills for precision B2B machining.
Running a high-grade carbide spot drill for aluminum too slow is just as damaging as running it too fast. When the feed rate is too light, the cutting edge rubs instead of cutting, generating friction heat that promotes chip welding.
To calculate rotational spindle speed (RPM) from surface speed:
RPM = (Surface Feet per Minute × 3.82) / Tool Diameter in Inches
Or using metric surface speed (V_c in meters per minute):
RPM = (V_c × 1000) / (3.1416 × Tool Diameter in Millimeters)
To determine the CNC table plunge feed rate (Inches Per Minute):
Feed Rate (IPM) = Spindle RPM × Number of Flutes × Chip Load per Tooth (IPT)
Programming Rule: Do Not Dwell on Aluminum!
Many programmers routinely call a G82 cycle with a 0.3 to 0.5-second dwell at the bottom of the cut to burnish the chamfer. In aluminum, dwelling rubs the carbide against the workpiece, generating friction, rubbing off your sharp edge, and welding aluminum to the tip. Always use a standard G81 drill cycle with a direct retract. Let the mirror-polished cutting edge do the work on the way in, then pull right out.
Flood coolant should be aimed directly at the cut zone to clear chips from the dimple. If you run high-pressure through-coolant or air-mist MQL setups, verify your coolant pressure is adequate to blow chips clear of the pocket before the spindle moves to the next X-Y coordinate.
For reference on drilling mechanics, tool wear patterns, and standard drill geometries, see comprehensive manufacturing resources like Wikipedia’s drill bit engineering guide.
When buying tooling in production quantities, purchasing managers must look beyond glossy marketing brochures. Use this engineering checklist when evaluating an industrial spot drill manufacturer:
If you are standardizing your tool crib or troubleshooting persistent hole-quality problems, you can always reach out to our engineering team for technical guidance, CAD drawings, or custom tool quotes.
A carbide spot drill for aluminum works best when supported by reliable toolholders and complementary tooling across your machining setup:
Combining quality tool holding with purpose-built CNC aluminum tools creates a stable, repeatable holemaking process that runs smoothly shift after shift.
Center drills feature a stepped pilot tip followed by a 60-degree countersink cone, originally developed to create clearance holes for lathe live centers. That thin pilot tip is fragile and prone to snapping if subjected to side loads or fast plunges on a CNC mill. A carbide spot drill for aluminum has no stepped pilot—it uses a continuous conical point (such as 90°, 120°, or 142°) supported by a thick carbide core. It is far more rigid, handles higher feed rates, and will not snap in your workpiece.
AlTiN (Aluminum Titanium Nitride) coatings contain aluminum. When machining non-ferrous aluminum alloys, the chemical affinity between the aluminum in the workpiece and the aluminum in the tool coating causes the material to weld together under cutting heat. That chemical bonding leads to severe built-up edge and chipped tools. In aluminum, you should use an uncoated, mirror-polished carbide spot drill for aluminum, or tools coated with non-affinity materials like DLC (Diamond-Like Carbon) or TiB2 (Titanium Diboride).
Modern solid carbide twist drills with web-thinned points can often drill without a pilot hole on flat surfaces up to 3x to 5x diameter depths. However, you should always use an aluminum spotting drill if:
1. The hole enters an irregular, angled, or curved surface (such as a round billet or cast skin).
2. You must hold an exacting true position tolerance (under 0.025 mm / 0.001 in).
3. You are running long-reach drills (8xD or deeper) that require a stable pilot pocket to prevent deflection.
Heavy burrs usually stem from three issues: using a blunt or unthinned chisel edge that displaces material rather than shearing it, feeding too slowly so the tool rubs, or dwelling at the bottom of the cut with a G82 cycle. To achieve burr-free holes, use a sharp, mirror-polished carbide spot drill for aluminum, maintain an aggressive chip load, and program an immediate G81 retract.
Tired of fighting chip buildup, erratic hole walk, and broken carbide drills on your aluminum production lines?
At Durable Mills, we grind our solid carbide spot drill for aluminum family to exacting tolerances. Using premium sub-micron virgin tungsten carbide, optimized clearance angles, and proprietary mirror-polished flutes (Ra < 0.08 µm), our spotting tools deliver clean entries and consistent hole locations across demanding production environments.


