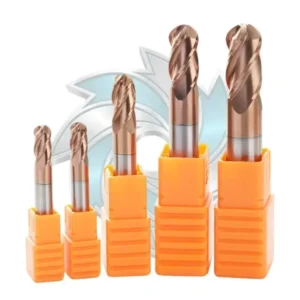
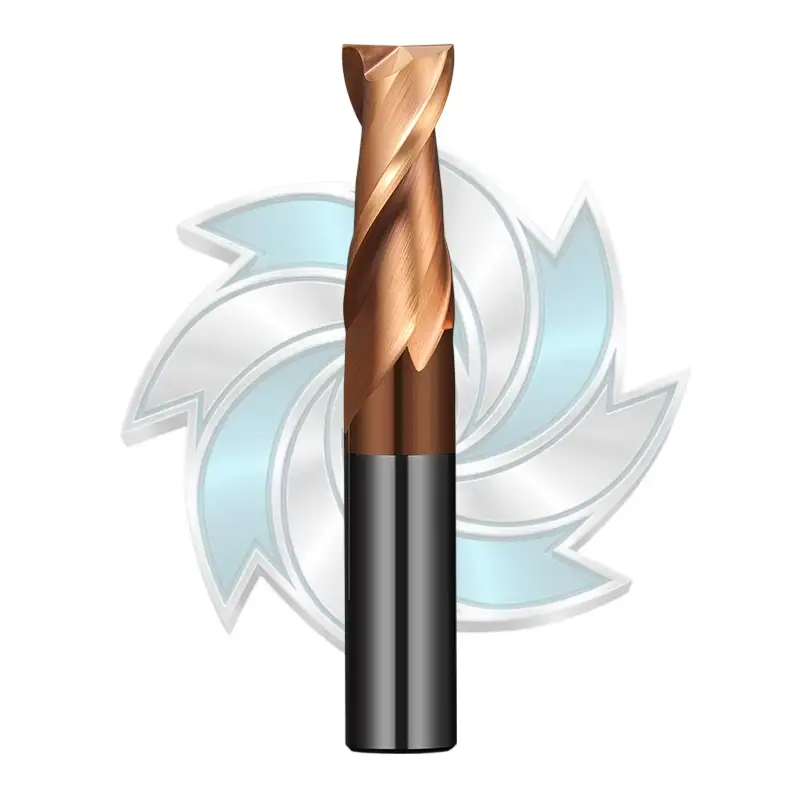
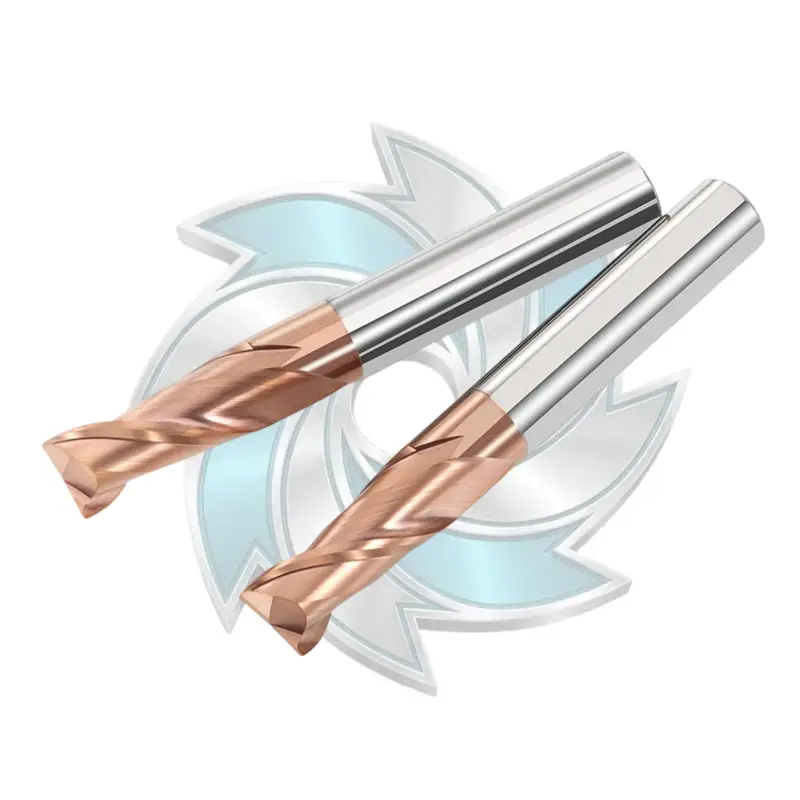
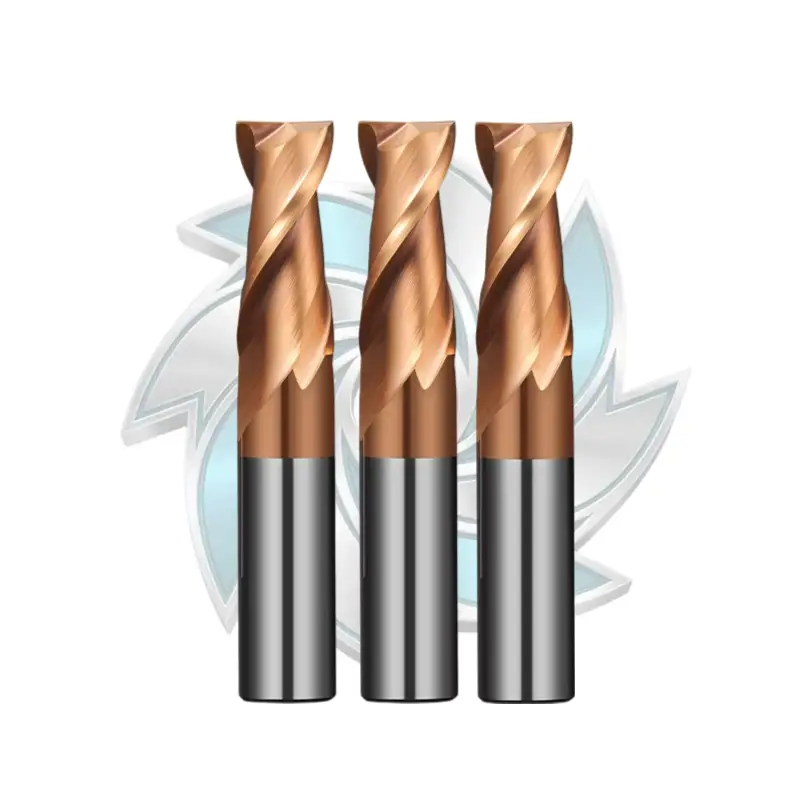
Engineered and manufactured by Durable Mills, this HRC55 2 flute carbide end mill is an economical, high-performance universal milling cutter designed for demanding CNC machining. Built with a premium 10% Cobalt micro-grain tungsten carbide substrate (HRA 91.2–91.7), it delivers extraordinary edge retention, superior thermal stability, and maximum wear resistance when machining carbon steels, alloy steels, and cast iron up to HRC 55.
| ISO Group | Workpiece Material | Machinability & Application Status |
|---|---|---|
| P (Steel) | Carbon Steel / Alloy Steel (<35 HRC) Alloy Steel (35–48 HRC) |
Primary recommendation. Optimal tool life and surface finish. |
| M (Stainless) | Stainless Steels | Applicable under controlled cutting speed and proper coolant supply. |
| K (Cast Iron) | Gray Cast Iron / Ductile Cast Iron (<32 HRC) | Primary recommendation. Exceptional resistance to abrasive dust wear. |
| N (Non-Ferrous) | Aluminum Alloy / Copper Alloy | Suitable for multi-material workshops and general-purpose light profiling. |
| H (Hardened) | Alloy Steel / Hardened Steel (45–55 HRC, max 65 HRC) | Recommended up to HRC 55; adjust parameters according to material hardness. |
| Workpiece Material | Axial Depth of Cut (ap) | Radial Width of Cut (ae) | Cutting Speed (Vc) | Feed per Tooth (fz) |
|---|---|---|---|---|
| Carbon Steel & Alloy Steel (<35 HRC) | ap ≤ 1.5D | ae ≤ 0.15D | 170 m/min | 0.008D mm/z |
| Gray Cast Iron & Ductile Iron (<32 HRC) | ap ≤ 1.5D | ae ≤ 0.15D | 150 m/min | 0.0065D mm/z |
| Alloy Steel / Hardened Steel (45–55 HRC) | ap ≤ 0.5D | ae ≤ 0.05D | 80–120 m/min | 0.004D mm/z |
*Note: Please adjust feed rates and cutting speeds according to workpiece rigidity, machine tool stability, and coolant conditions.
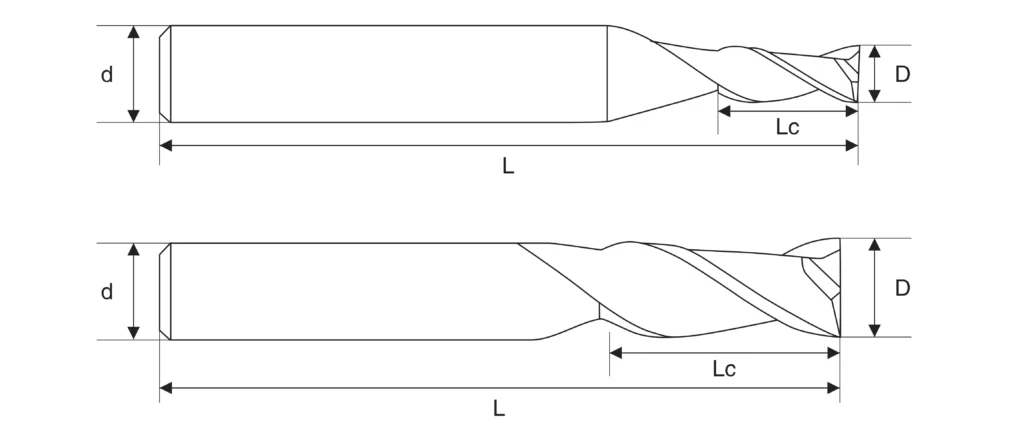
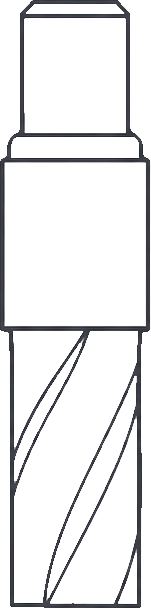
| No. | Model Designation | Cutting Dia. (D) | Flute Length (Lc) | Shank Dia. (d) | Overall Length (L) | Flutes (T) |
|---|---|---|---|---|---|---|
| 1 | DM-3*8*3*50-2T | 3.0 mm | 8.0 mm | 3.0 mm | 50 mm | 2 |
| 2 | DM-3*12*3*75-2T | 3.0 mm | 12.0 mm | 3.0 mm | 75 mm | 2 |
| 3 | DM-3*15*3*100-2T | 3.0 mm | 15.0 mm | 3.0 mm | 100 mm | 2 |
| 4 | DM-1*3*4*50-2T | 1.0 mm | 3.0 mm | 4.0 mm | 50 mm | 2 |
| 5 | DM-1.5*4*4*50-2T | 1.5 mm | 4.0 mm | 4.0 mm | 50 mm | 2 |
| 6 | DM-2*5*4*50-2T | 2.0 mm | 5.0 mm | 4.0 mm | 50 mm | 2 |
| 7 | DM-2.5*7*4*50-2T | 2.5 mm | 7.0 mm | 4.0 mm | 50 mm | 2 |
| 8 | DM-3*8*4*50-2T | 3.0 mm | 8.0 mm | 4.0 mm | 50 mm | 2 |
| 9 | DM-3.5*10*4*50-2T | 3.5 mm | 10.0 mm | 4.0 mm | 50 mm | 2 |
| 10 | DM-4*10*4*50-2T | 4.0 mm | 10.0 mm | 4.0 mm | 50 mm | 2 |
| 11 | DM-4*16*4*75-2T | 4.0 mm | 16.0 mm | 4.0 mm | 75 mm | 2 |
| 12 | DM-4*20*4*100-2T | 4.0 mm | 20.0 mm | 4.0 mm | 100 mm | 2 |
| 13 | DM-1*3*4*75-2T | 1.0 mm | 3.0 mm | 4.0 mm | 75 mm | 2 |
| 14 | DM-1.5*4*4*75-2T | 1.5 mm | 4.0 mm | 4.0 mm | 75 mm | 2 |
| 15 | DM-2*5*4*75-2T | 2.0 mm | 5.0 mm | 4.0 mm | 75 mm | 2 |
| 16 | DM-2.5*7*4*75-2T | 2.5 mm | 7.0 mm | 4.0 mm | 75 mm | 2 |
| 17 | DM-3*8*4*75-2T | 3.0 mm | 8.0 mm | 4.0 mm | 75 mm | 2 |
| 18 | DM-5*13*5*50-2T | 5.0 mm | 13.0 mm | 5.0 mm | 50 mm | 2 |
| 19 | DM-5*20*5*75-2T | 5.0 mm | 20.0 mm | 5.0 mm | 75 mm | 2 |
| 20 | DM-5*25*5*100-2T | 5.0 mm | 25.0 mm | 5.0 mm | 100 mm | 2 |
| 21 | DM-1*3*6*50-2T | 1.0 mm | 3.0 mm | 6.0 mm | 50 mm | 2 |
| 22 | DM-1.5*4*6*50-2T | 1.5 mm | 4.0 mm | 6.0 mm | 50 mm | 2 |
| 23 | DM-2*5*6*50-2T | 2.0 mm | 5.0 mm | 6.0 mm | 50 mm | 2 |
| 24 | DM-2.5*7*6*50-2T | 2.5 mm | 7.0 mm | 6.0 mm | 50 mm | 2 |
| 25 | DM-3*8*6*50-2T | 3.0 mm | 8.0 mm | 6.0 mm | 50 mm | 2 |
| 26 | DM-3.5*10*6*50-2T | 3.5 mm | 10.0 mm | 6.0 mm | 50 mm | 2 |
| 27 | DM-4*10*6*50-2T | 4.0 mm | 10.0 mm | 6.0 mm | 50 mm | 2 |
| 28 | DM-4.5*12*6*50-2T | 4.5 mm | 12.0 mm | 6.0 mm | 50 mm | 2 |
| 29 | DM-5*13*6*50-2T | 5.0 mm | 13.0 mm | 6.0 mm | 50 mm | 2 |
| 30 | DM-6*15*6*50-2T | 6.0 mm | 15.0 mm | 6.0 mm | 50 mm | 2 |
| 31 | DM-6*25*6*75-2T | 6.0 mm | 25.0 mm | 6.0 mm | 75 mm | 2 |
| 32 | DM-6*30*6*100-2T | 6.0 mm | 30.0 mm | 6.0 mm | 100 mm | 2 |
| 33 | DM-6*40*6*150-2T | 6.0 mm | 40.0 mm | 6.0 mm | 150 mm | 2 |
| 34 | DM-7*18*8*60-2T | 7.0 mm | 18.0 mm | 8.0 mm | 60 mm | 2 |
| 35 | DM-8*20*8*60-2T | 8.0 mm | 20.0 mm | 8.0 mm | 60 mm | 2 |
| 36 | DM-8*28*8*75-2T | 8.0 mm | 28.0 mm | 8.0 mm | 75 mm | 2 |
Durable Mills is a dedicated manufacturer of precision solid carbide cutting tools. We support tool distributors, wholesalers, and CNC machining facilities worldwide with complete OEM solutions:
To request bulk pricing or discuss custom tool geometry, please visit our Contact Page or contact our engineering sales department via email at info@durablemills.com.
A: It is primarily designed for slotting, pocketing, plunging, and ramping operations on carbon steels, alloy steels, and cast iron up to HRC 55. The 2-flute configuration provides the chip clearance needed for deep slots without packing chips.
A: A negative rake angle strengthens the cutting edge by placing the tool material under compressive stress rather than shear stress, significantly reducing the likelihood of edge chipping during interrupted cuts or when machining pre-hardened steel.
A: It balances high wear resistance (HRA 91.2–91.7) with versatile substrate chemistry (10% Cobalt), allowing job shops to machine carbon steel, cast iron, and pre-hardened mold steel with a single, cost-effective tool type.
A: Yes. In addition to our 36 standard catalogue sizes, we manufacture custom dimensions, step tools, and specialized coatings to your exact engineering drawings.
A: Individual tools are packaged in protective square plastic tubes. Standard stock items ship within 24 to 48 hours, while custom OEM production runs typically dispatch in 10 to 15 business days. Inquire via our Contact Page for immediate inventory checks.