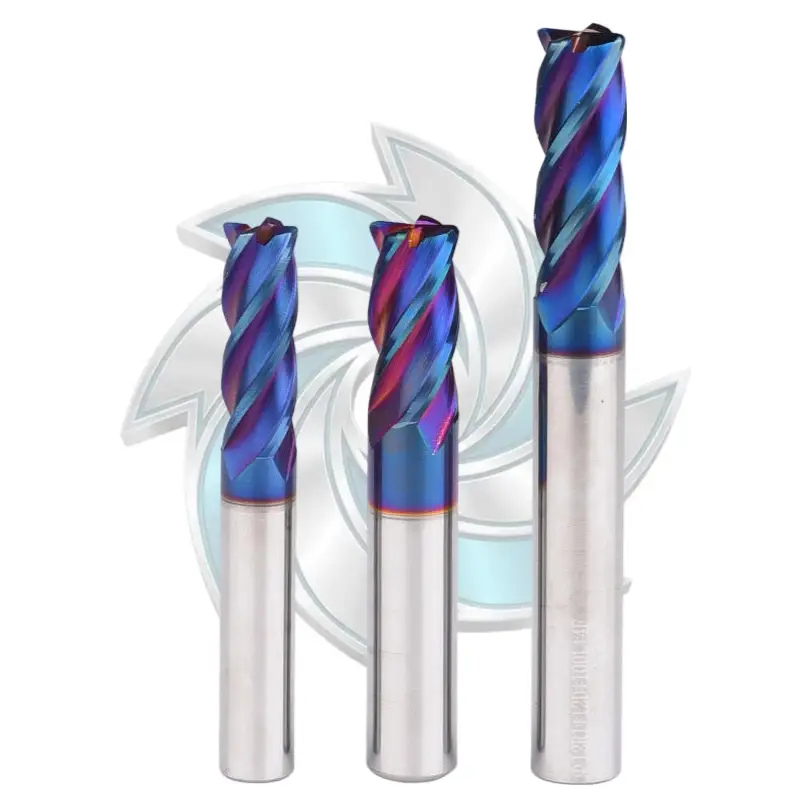
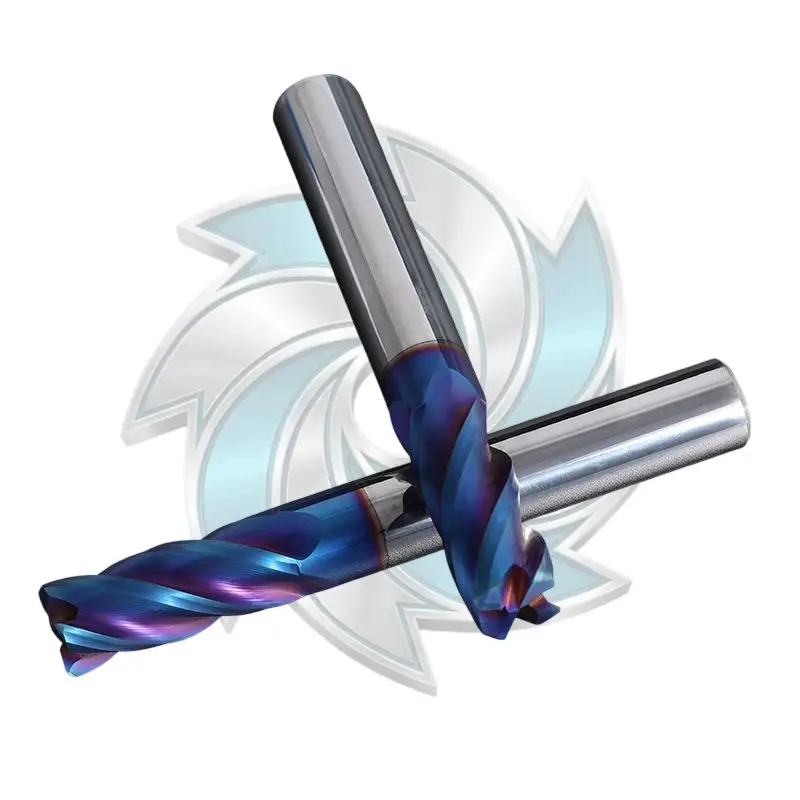
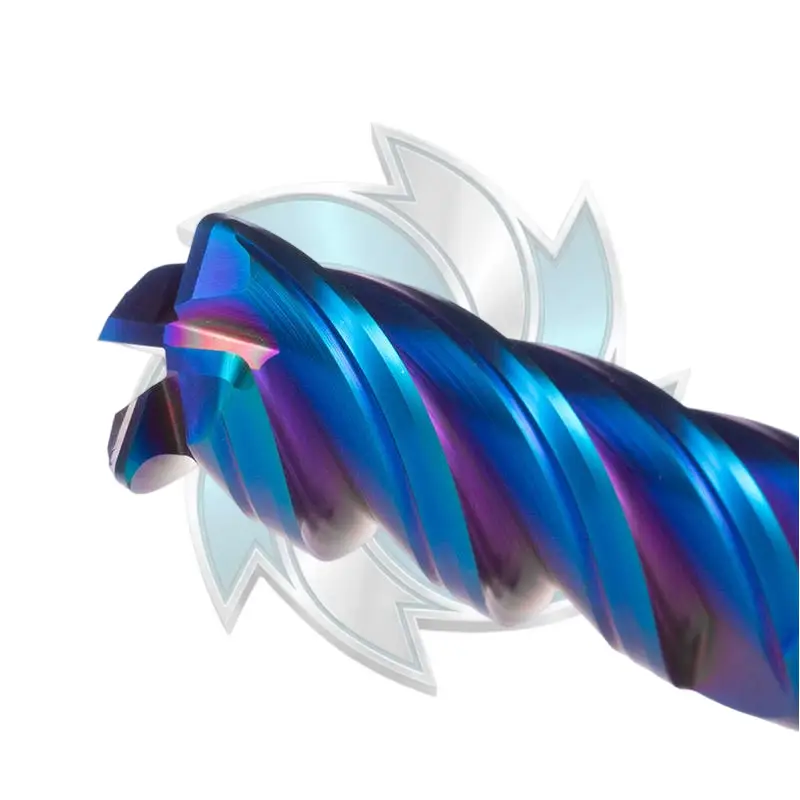
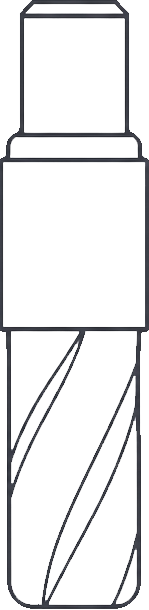

Engineered and supplied by Durable Mills, this professional-grade bull nose end mill is crafted for high-performance profiling, semi-finishing, and cavity milling in tough alloys and hardened steels up to HRC65. Built on an ultra-fine 0.4 µm tungsten carbide substrate with 12% cobalt content (HRA 92.5–93), this 4-flute tool features rounded R-cutting edges that disperse cutting forces effectively, drastically reducing edge chipping and thermal failure.
| Parameter | Specification Value |
|---|---|
| Tool Structure | 4 Flute Solid Carbide Bull Nose End Mill |
| Applicable Workpiece Hardness | Up to HRC65 |
| Cobalt Content (Co) | 12% |
| Grain Size | 0.4 µm (Sub-micron Solid Carbide) |
| Substrate Hardness | HRA 92.5 – 93.0 |

| Model Number | Cutting Dia. (D) | Flute Length (Lc) | Shank Dia. (d) | Overall Length (L) | Corner Radius (R) | Flutes |
|---|---|---|---|---|---|---|
| DM-3*8*3*50*4T | 3 mm | 8 mm | 3 mm | 50 mm | R0.5 / R1.0 | 4 |
| DM-3*12*3*75L*4T | 3 mm | 12 mm | 3 mm | 75 mm | R0.5 / R1.0 | 4 |
| DM-3*15*3*100*4T | 3 mm | 15 mm | 3 mm | 100 mm | R0.5 / R1.0 | 4 |
| DM-1*3*4*50*4T | 1 mm | 3 mm | 4 mm | 50 mm | R0.2 | 4 |
| DM-1.5*4*4*50*4T | 1.5 mm | 4 mm | 4 mm | 50 mm | R0.2 | 4 |
| DM-2*5*4*50*4T | 2 mm | 5 mm | 4 mm | 50 mm | R0.2 / R0.5 | 4 |
| DM-3*8*4*50*4T | 3 mm | 8 mm | 4 mm | 50 mm | R0.2 / R0.5 / R1.0 | 4 |
| DM-4*10*4*50*4T | 4 mm | 10 mm | 4 mm | 50 mm | R0.2 / R0.5 / R1.0 | 4 |
| DM-4*16*4*75*4T | 4 mm | 16 mm | 4 mm | 75 mm | R0.5 / R1.0 | 4 |
| DM-4*20*4*100*4T | 4 mm | 20 mm | 4 mm | 100 mm | R0.5 / R1.0 | 4 |
| DM-5*13*5*50*4T | 5 mm | 13 mm | 5 mm | 50 mm | R0.5 / R1.0 | 4 |
| DM-5*20*5*75*4T | 5 mm | 20 mm | 5 mm | 75 mm | R0.5 / R1.0 | 4 |
| DM-5*25*5*100*4T | 5 mm | 25 mm | 5 mm | 100 mm | R0.5 / R1.0 | 4 |
| DM-6*15*6*50*4T | 6 mm | 15 mm | 6 mm | 50 mm | R0.2 / R0.5 / R1.0 | 4 |
| DM-6*13*6*50*4T | 6 mm | 13 mm | 6 mm | 50 mm | R0.5 / R1.0 | 4 |
| DM-6*25*6*75*4T | 6 mm | 25 mm | 6 mm | 75 mm | R0.5 / R1.0 | 4 |
| DM-6*30*6*100*4T | 6 mm | 30 mm | 6 mm | 100 mm | R0.5 / R1.0 | 4 |
| DM-6*40*6*150*4T | 6 mm | 40 mm | 6 mm | 150 mm | R0.5 / R1.0 | 4 |
| DM-8*20*8*60*4T | 8 mm | 20 mm | 8 mm | 60 mm | R0.2 / R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-8*28*8*75*4T | 8 mm | 28 mm | 8 mm | 75 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-8*35*8*100*4T | 8 mm | 35 mm | 8 mm | 100 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-8*50*8*150*4T | 8 mm | 50 mm | 8 mm | 150 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-10*25*10*75*4T | 10 mm | 25 mm | 10 mm | 75 mm | R0.2 / R0.5 / R1.0 / R1.5 / R2.0 / R3.0 | 4 |
| DM-10*40*10*100*4T | 10 mm | 40 mm | 10 mm | 100 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-10*50*10*150*4T | 10 mm | 50 mm | 10 mm | 150 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-12*30*12*75*4T | 12 mm | 30 mm | 12 mm | 75 mm | R0.2 / R0.5 / R1.0 / R1.5 / R2.0 / R3.0 | 4 |
| DM-12*45*12*100*4T | 12 mm | 45 mm | 12 mm | 100 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| DM-12*60*12*150*4T | 12 mm | 60 mm | 12 mm | 150 mm | R0.5 / R1.0 / R2.0 / R3.0 | 4 |
| Workpiece Material | Axial Depth (ap) | Radial Width (ae) | Cutting Speed (Vc: m/min) | Feed per Tooth (fz: mm/z) |
|---|---|---|---|---|
| Carbon Steel, Alloy Steel (<35 HRC) | ap ≤ 1.5D | ae ≤ 0.1D | 120 | 0.006D |
| Alloy Steel (35–48 HRC) | ap ≤ 1.5D | ae ≤ 0.1D | 80 | 0.0035D |
| Stainless Steels | ap ≤ 1.5D | ae ≤ 0.1D | 100 | 0.006D |
| Gray Cast Iron, Ductile Cast Iron (<32 HRC) | ap ≤ 1.5D | ae ≤ 0.1D | 120 | 0.0055D |
| Hardened Steel (45–65 HRC) | Fine stepdown | ae ≤ 0.05D | 60 – 90 | 0.002D – 0.004D |
*Note: Please adjust operating parameters based on machine tool rigidity, tool overhang, and clamping stability.
Q1: What are the primary machining advantages of using a bull nose end mill?
A1: A bull nose end mill combines the flat bottom of a square cutter with the edge durability of a radius tip. It distributes cutting stress away from vulnerable points, enabling higher feed rates, reduced tool deflection, and smooth blending in mold cavities.
Q2: What is the minimum wholesale order and delivery timeline?
A2: We maintain regular inventory for standard metric sizes ready for immediate export dispatch within 48 hours. For OEM packaging or tailored batches, reach out via our contact page or directly at info@durablemills.com.
Q3: How does this tool perform on pre-hardened steels and ductile irons?
A3: Thanks to the high-density micro-grain carbide matrix (12% Co) and nano heat-shield coating, it delivers continuous wear resistance and stable chip evacuation in materials up to HRC65 without micro-fracturing.
Q4: Can Durable Mills provide custom shank lengths or tailored corner radii?
A4: Yes, we provide full ODM and OEM customization, including extra-long overall lengths, necked-down reaches, and bespoke corner radius dimensions suited to your workpiece drawings.