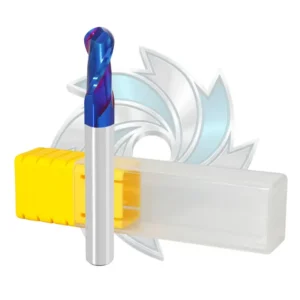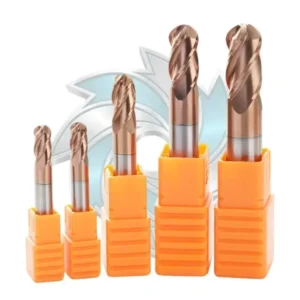
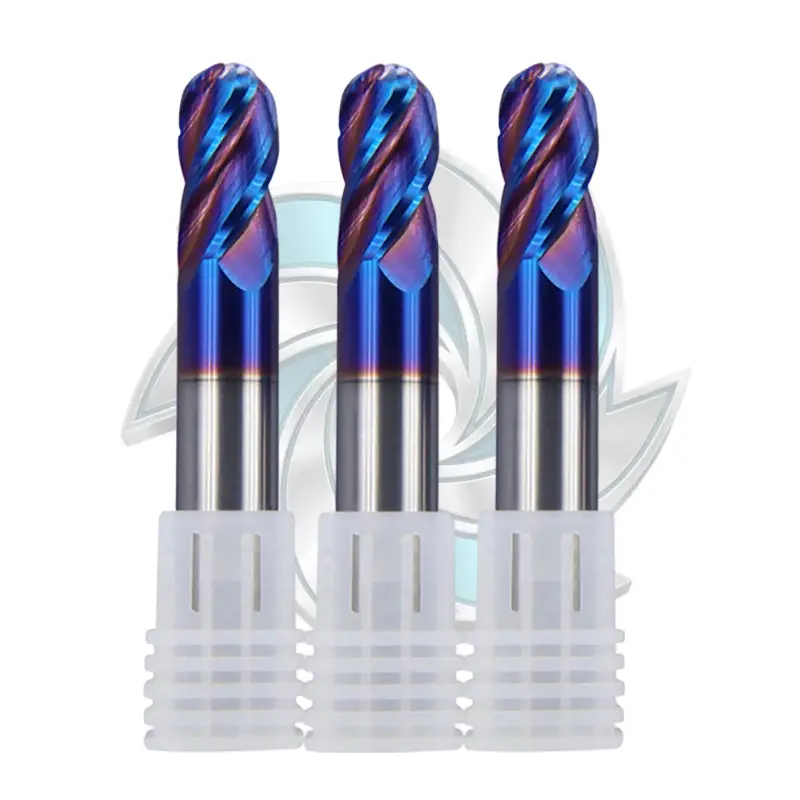
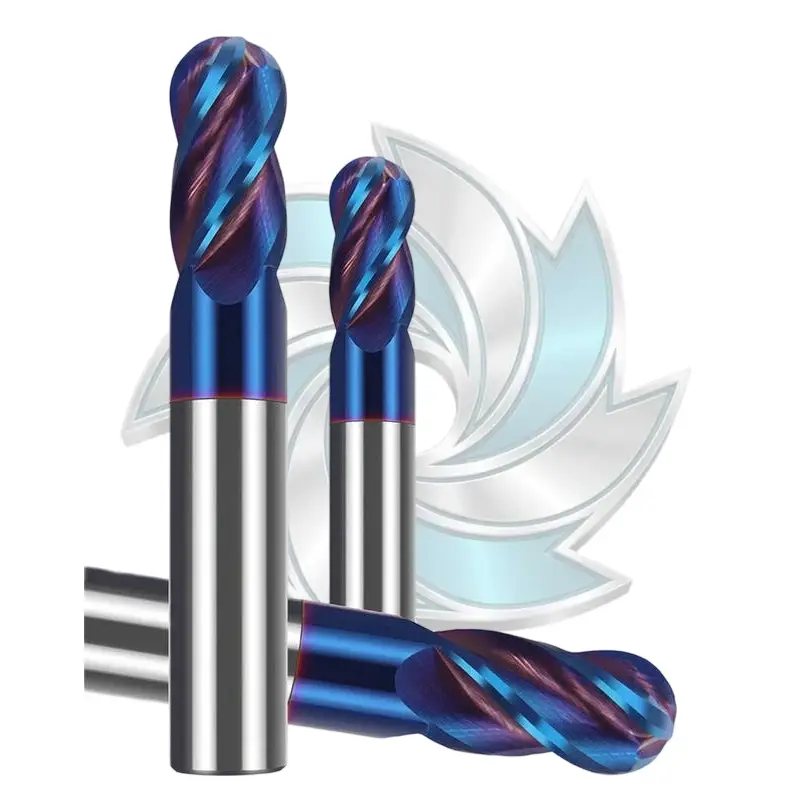
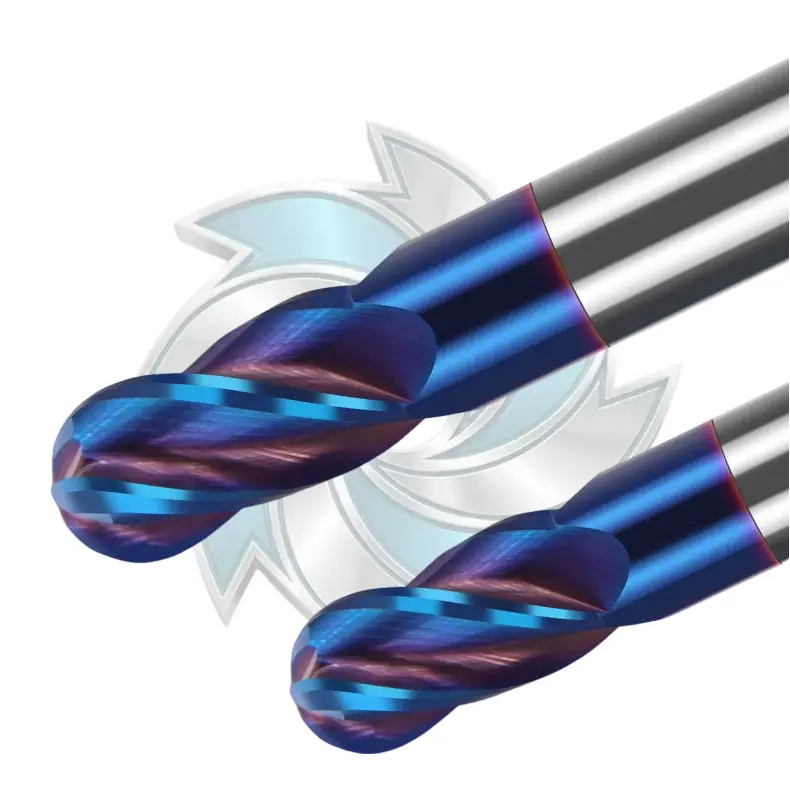
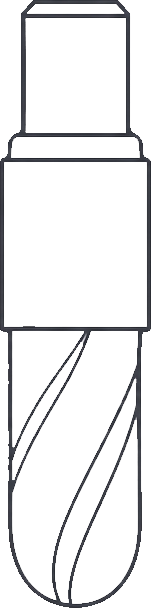

Designed by Durable Mills, this industrial-grade HRC65 ball nose end mill is engineered for high-precision 3D profiling, contouring, and finishing in demanding toolroom applications. Built from ultra-fine 0.4 μm micro-grain carbide with a 12% cobalt matrix, this solid carbide cutter provides outstanding hardness (HRA 92.5–93) and extreme wear resistance when machining heat-treated steels up to 65 HRC.

| Property / Element | Specification |
|---|---|
| Cobalt Content (Co) | 12% |
| Grain Size | 0.4 μm Micro-grain |
| Substrate Hardness | HRA 92.5 – 93 |
| Workpiece Hardness Range | Up to 65 HRC |
| Model Number | Radius (R, mm) | Flute Length (Lc, mm) | Shank Dia (d, mm) | Overall Length (L, mm) | Flutes |
|---|---|---|---|---|---|
| DM-R1.5*6*3*50*4T | 1.5 | 6 | 3 | 50 | 4 |
| DM-R1.5*6*3*75*4T | 1.5 | 6 | 3 | 75 | 4 |
| DM-R1.5*6*3*100*4T | 1.5 | 6 | 3 | 100 | 4 |
| DM-R0.5*2*4*50*4T | 0.5 | 2 | 4 | 50 | 4 |
| DM-R0.75*3*4*50*4T | 0.75 | 3 | 4 | 50 | 4 |
| DM-R1*4*4*50*4T | 1.0 | 4 | 4 | 50 | 4 |
| DM-R1.25*5*4*50*4T | 1.25 | 5 | 4 | 50 | 4 |
| DM-R1.5*6*4*50*4T | 1.5 | 6 | 4 | 50 | 4 |
| DM-R1.75*7*4*50*4T | 1.75 | 7 | 4 | 50 | 4 |
| DM-R2*8*4*50*4T | 2.0 | 8 | 4 | 50 | 4 |
| DM-R2*8*4*75*4T | 2.0 | 8 | 4 | 75 | 4 |
| DM-R2*8*4*100*4T | 2.0 | 8 | 4 | 100 | 4 |
| DM-R2.5*10*5*50*4T | 2.5 | 10 | 5 | 50 | 4 |
| DM-R2.5*10*5*75*4T | 2.5 | 10 | 5 | 75 | 4 |
| DM-R2.5*10*5*100*4T | 2.5 | 10 | 5 | 100 | 4 |
| DM-R2.5*10*6*50*4T | 2.5 | 10 | 6 | 50 | 4 |
| DM-R3*12*6*50*4T | 3.0 | 12 | 6 | 50 | 4 |
| DM-R3*12*6*75*4T | 3.0 | 12 | 6 | 75 | 4 |
| DM-R3*12*6*100*4T | 3.0 | 12 | 6 | 100 | 4 |
| DM-R3*12*6*150*4T | 3.0 | 12 | 6 | 150 | 4 |
| DM-R3.5*14*8*60*4T | 3.5 | 14 | 8 | 60 | 4 |
| DM-R4*16*8*60*4T | 4.0 | 16 | 8 | 60 | 4 |
| DM-R4*16*8*75*4T | 4.0 | 16 | 8 | 75 | 4 |
| DM-R4*16*8*100*4T | 4.0 | 16 | 8 | 100 | 4 |
| DM-R4*16*8*150*4T | 4.0 | 16 | 8 | 150 | 4 |
| DM-R4.5*18*10*75*4T | 4.5 | 18 | 10 | 75 | 4 |
| DM-R5*20*10*75*4T | 5.0 | 20 | 10 | 75 | 4 |
| DM-R5*20*10*100*4T | 5.0 | 20 | 10 | 100 | 4 |
| DM-R5*20*10*150*4T | 5.0 | 20 | 10 | 150 | 4 |
| DM-R5.5*22*12*75*4T | 5.5 | 22 | 12 | 75 | 4 |
| DM-R6*24*12*75*4T | 6.0 | 24 | 12 | 75 | 4 |
| DM-R6*24*12*100*4T | 6.0 | 24 | 12 | 100 | 4 |
| DM-R6*24*12*150*4T | 6.0 | 24 | 12 | 150 | 4 |
| DM-R6.5*26*14*100*4T | 6.5 | 26 | 14 | 100 | 4 |
| DM-R7*28*14*80*4T | 7.0 | 28 | 14 | 80 | 4 |
| DM-R7*28*14*100*4T | 7.0 | 28 | 14 | 100 | 4 |
| ISO / Material Group | Axial Depth (ap) | Radial Width (ae) | Cutting Speed (Vc, m/min) | Feed per Tooth (fz, mm/z) |
|---|---|---|---|---|
| P Carbon Steel, Alloy Steel (<35 HRC) | ap ≤ 0.2D | ae ≤ 0.2D | 120 | 0.004D |
| P Alloy Steel (35–48 HRC) | ap ≤ 0.1D | ae ≤ 0.1D | 80 | 0.004D |
| M Stainless Steels | ap ≤ 0.2D | ae ≤ 0.2D | 80 | 0.004D |
| K Gray Cast Iron, Ductile Cast Iron (<32 HRC) | ap ≤ 0.2D | ae ≤ 0.2D | 120 | 0.004D |
| H Alloy Steel, Hardened Steel (45–65 HRC) | Adjust based on hardness | Adjust based on hardness | 60 – 100 | 0.003D – 0.004D |
The negative rake angle reinforces the tool’s cutting edge by redirecting cutting forces into the solid carbide body. This significantly reduces micro-chipping and flank breakage when high-speed cutting hard materials up to 65 HRC.
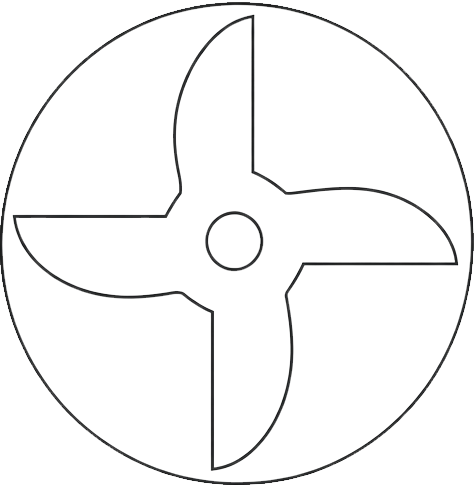
While capable of light roughing and semi-finishing, this 4-flute ball nose end mill excels at semi-finishing and high-precision 3D surface finishing, where surface roughness and tight profile tolerances are critical.
Yes. Durable Mills provides full OEM/ODM services, including customized overall lengths, extended reaches, specialized PVD coatings, and custom shank branding for wholesale distributors.
You can contact our sales engineering team directly via our contact page or email us at info@durablemills.com for volume quotes and test samples.