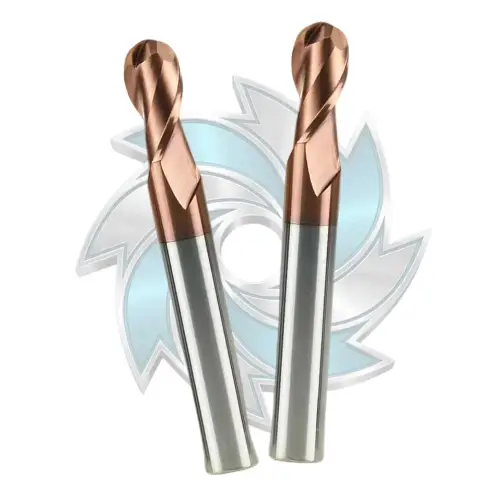
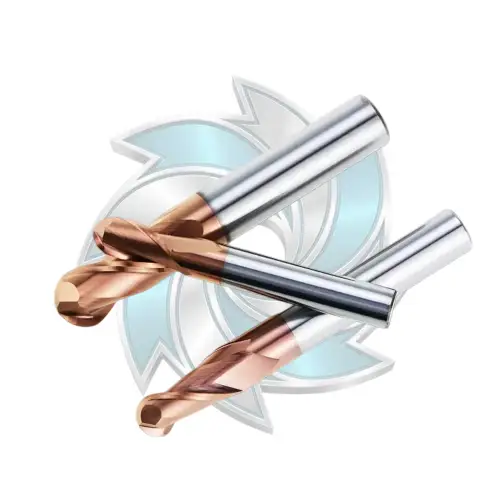
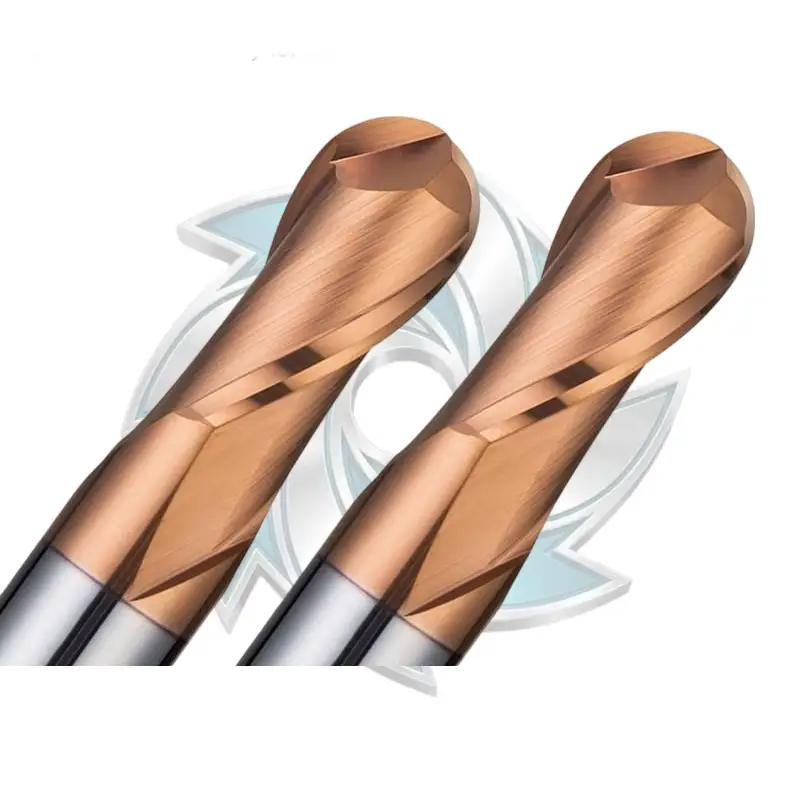
Manufactured by Durable Mills, this industrial-grade 2 flute ball nose end mill is engineered specifically for finishing and semi-finishing operations on hardened steel, chilled cast iron, and high-tensile alloy steels up to HRC68. Compared to standard multi-flute tools, the optimized 2-flute ball nose geometry provides superior contouring accuracy, larger chip evacuation space, and reduced vibration during high-speed 3D copy milling and complex cavity profiling.
| Parameter | Specification Value |
|---|---|
| Cobalt Content (Co) | 9% – 10% |
| Grain Size | 0.3 μm – 0.4 μm (Ultra Micro-grain) |
| Hardness (HRA) | HRA 93.2 – 94.0 |
| Working Hardness Range | Up to HRC 68 |
| Helix Angle / Flutes | 30° / 2 Flutes |
| Workpiece Material | Axial Depth (ap) | Radial Width (ae) | Linear Speed Vc (m/min) | Feed Rate fz (mm/z) |
|---|---|---|---|---|
| Alloy Steel, Hardened Steel (45-65 HRC) | ap ≤ 0.05-0.1D | ae ≤ 0.02D | 70 – 100 | 0.015D |
| Hardened Steel & Chilled Cast Iron (>65 HRC) | ap ≤ 0.03-0.08D | ae ≤ 0.015D | 60 – 90 | 0.010D |
| Carbon Steel & Alloy Steel (<35 HRC) | ap ≤ 0.15D | ae ≤ 0.05D | 120 – 180 | 0.025D |
| Stainless Steel & Cast Iron (<32 HRC) | ap ≤ 0.1D | ae ≤ 0.03D | 80 – 120 | 0.018D |

| Model Code | Radius R (mm) | Flute Length Lc (mm) | Shank Dia. d (mm) | Total Length L (mm) | Flutes |
|---|---|---|---|---|---|
| DM-R1.5*6*3*50*2T | 1.5 | 6 | 3 | 50 | 2 |
| DM-R1.5*6*3*75*2T | 1.5 | 6 | 3 | 75 | 2 |
| DM-R1.5*6*3*100*2T | 1.5 | 6 | 3 | 100 | 2 |
| DM-R0.5*2*4*50*2T | 0.5 | 2 | 4 | 50 | 2 |
| DM-R0.75*3*4*50*2T | 0.75 | 3 | 4 | 50 | 2 |
| DM-R1*4*4*50*2T | 1.0 | 4 | 4 | 50 | 2 |
| DM-R1.25*5*4*50*2T | 1.25 | 5 | 4 | 50 | 2 |
| DM-R1.5*6*4*50*2T | 1.5 | 6 | 4 | 50 | 2 |
| DM-R1.75*7*4*50*2T | 1.75 | 7 | 4 | 50 | 2 |
| DM-R2*8*4*50*2T | 2.0 | 8 | 4 | 50 | 2 |
| DM-R2*8*4*75*2T | 2.0 | 8 | 4 | 75 | 2 |
| DM-R2*8*4*100*2T | 2.0 | 8 | 4 | 100 | 2 |
| DM-R2.5*10*5*50*2T | 2.5 | 10 | 5 | 50 | 2 |
| DM-R2.5*10*5*75*2T | 2.5 | 10 | 5 | 75 | 2 |
| DM-R2.5*10*5*100*2T | 2.5 | 10 | 5 | 100 | 2 |
| DM-R2.5*10*6*50*2T | 2.5 | 10 | 6 | 50 | 2 |
| DM-R3*12*6*50*2T | 3.0 | 12 | 6 | 50 | 2 |
| DM-R3*12*6*75*2T | 3.0 | 12 | 6 | 75 | 2 |
| DM-R3*12*6*100*2T | 3.0 | 12 | 6 | 100 | 2 |
| DM-R3*12*6*150*2T | 3.0 | 12 | 6 | 150 | 2 |
| DM-R3.5*14*8*60*2T | 3.5 | 14 | 8 | 60 | 2 |
| DM-R4*16*8*60*2T | 4.0 | 16 | 8 | 60 | 2 |
| DM-R4*16*8*75*2T | 4.0 | 16 | 8 | 75 | 2 |
| DM-R4*16*8*100*2T | 4.0 | 16 | 8 | 100 | 2 |
| DM-R4*16*8*150*2T | 4.0 | 16 | 8 | 150 | 2 |
| DM-R4.5*18*10*75*2T | 4.5 | 18 | 10 | 75 | 2 |
| DM-R5*20*10*75*2T | 5.0 | 20 | 10 | 75 | 2 |
| DM-R5*20*10*100*2T | 5.0 | 20 | 10 | 100 | 2 |
| DM-R5*20*10*150*2T | 5.0 | 20 | 10 | 150 | 2 |
| DM-R5.5*22*12*75*2T | 5.5 | 22 | 12 | 75 | 2 |
| DM-R6*24*12*75*2T | 6.0 | 24 | 12 | 75 | 2 |
| DM-R6*24*12*100*2T | 6.0 | 24 | 12 | 100 | 2 |
| DM-R6*24*12*150*2T | 6.0 | 24 | 150 | 2 | |
| DM-R6.5*26*14*100*2T | 6.5 | 26 | 14 | 100 | 2 |
| DM-R7*28*14*80*2T | 7.0 | 28 | 14 | 80 | 2 |
| DM-R7*28*14*100*2T | 7.0 | 28 | 14 | 100 | 2 |
A 2 flute ball nose end mill offers significantly more chip pocket volume and eliminates tool center clearance interference during 3D copying. This ensures superior contour precision, smoother chip evacuation, and lower heat accumulation when finishing high-hardness steels.
This ball nose series is specifically engineered for workpieces up to HRC 68, including pre-hardened mold steel, tool steels, quenched steels, and chilled cast iron.
Yes. As a direct industrial manufacturer, Durable Mills supports OEM branding, custom shank/neck designs, custom overall lengths, and bulk wholesale pricing for international distributors.
For machining hardened steels above HRC 60, dry cutting with compressed air blow or oil mist (MQL) is highly recommended to avoid thermal shock and edge micro-chipping caused by flood coolant.
Contact our CNC tooling engineers today to discuss standard stock orders, OEM requirements, or tailored milling parameters.
Contact Durable Mills Sales →
Direct Email: info@durablemills.com